Ribbed-wall Silicon-core Microduct Production Line
Two-layer co-extrusion line for ribbed-wall silicon-core microduct in 14/10, 25/20 and 32/28 mm, combining high ring stiffness with low material weight.
Production line introduction
How the Ribbed-wall Silicon-core Microduct Production Line is engineered, and which sub-assemblies protect the duct properties your customers actually buy.
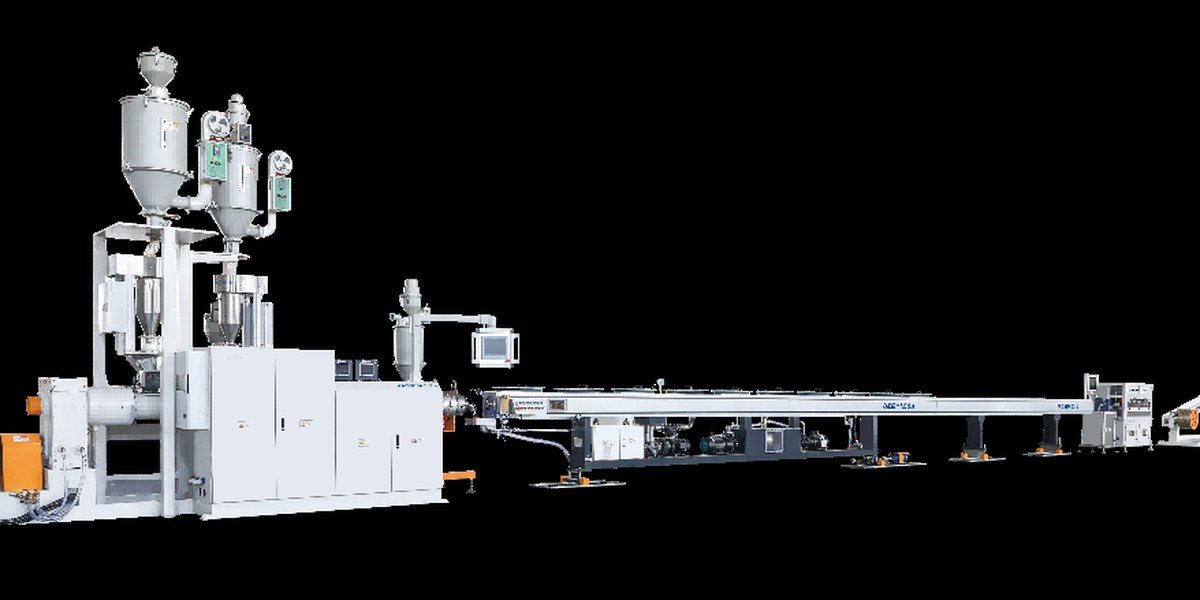
The ribbed-wall line runs two extruders into one co-extrusion die head: a high-speed extruder forming the ribbed HDPE outer wall, and a second extruder for the inner silicone layer. Forming the wall with ribs raises ring stiffness and crush resistance while saving material compared with a smooth wall of the same stiffness.
The microduct is calibrated on a specialised high-speed calibrator, cooled in a vacuum calibrating tank and a series of immersion tanks, then dried, hauled off on a servo belt haul-off and coiled on a servo-traversing winder. The tooling set covers the 14/10, 25/20 and 32/28 mm microduct sizes.
Machine set composition
Every line is quoted as a complete set. The main assemblies below are included in the supply.
| No. | Machine set composition | Qty. |
|---|---|---|
| 1 | SJ-60/36 high speed Extruder for HDPE | 1 set |
| 2 | SJ45/30 Extruder for Inner Silicon Layer | 1 set |
| 3 | XAL-300 Automatic Loader | 2sets |
| 4 | XBD-75/50 Hot Air Dryer | 1set/1set |
| 5 | High Speed Two Layers Co-extrusion Precision die head moulds | 1 set |
| 6 | Specialized High Speed Calibrator | 3units |
| 7 | SGZL-63 Vacuum Calibrating Cooling Stand | 1 set |
| 8 | SGL-63 Water Cooling Tank | 3 sets |
| 9 | Dehydration drying unit | 1 set |
| 10 | PQ-300 High-speed Belt Haul-off Machine | 1 set |
| 11 | SGJ-1300 Pipe Winder Machine | 1 set |
| 12 | Siemens PLC programmable computer control system | 1 set |
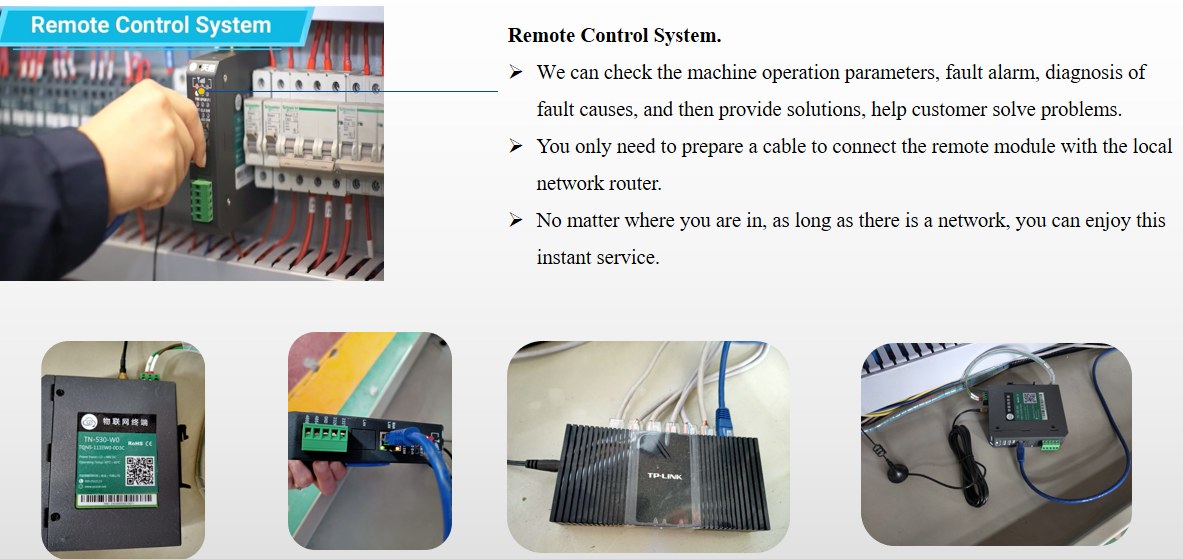
| 13 | Remote Control System | 1set |
Production line technical advantages
Each sub-assembly is selected to protect the properties your customers buy: blowing friction, diameter tolerance, roundness and coil quality.
Two-extruder co-extrusion
A dedicated HDPE extruder and a separate silicone extruder feed one precision two-layer die head, so wall geometry and the inner layer are controlled independently.
Ribbed-wall forming die
The ribbed outer wall is formed in the die head and fixed by vacuum calibration, raising ring stiffness for the same wall weight.
Specialised high-speed calibrator
Three calibrator units cover the 14/10 to 32/28 mm range and hold diameter and ovality at production speed.
Vacuum and immersion cooling
A vacuum calibrating stand and a series of water-immersion tanks give progressive cooling of the ribbed wall without distortion.
Servo haul-off and coiling
Belt haul-off with encoder length metering and a servo-traversing winder, so coil build-up stays even at production speed.
Siemens PLC line control
Synchronised control of both extruders, vacuum, haul-off and winder, with remote fault diagnosis and a Siemens operator panel in English.
Process flow
From raw material to packed coil, every station is matched in capacity so the line runs at the rated speed without a bottleneck.
- Raw material feeding and drying
- HDPE and silicone compound extrusion
- Two-layer co-extrusion die head
- Rib forming and vacuum calibration
- Immersion cooling
- Dehydration drying
- Belt haul-off
- Coiling
- Coil packing
Wide applicability
Typical end uses for the duct and bundle this line produces, based on the applications BENK equipment already serves worldwide.
Air-blown fibre microduct
Ribbed-wall microduct for air-blown fibre where stiffness and low blowing friction are both required.
Dense duct routes
Microduct routes that need higher crush resistance in crowded ducts, chambers and cabinets.
Direct-buried microduct
Ribbed-wall duct for direct burial and short-span ducting, where additional stiffness replaces heavy wall thickness.
Options and auxiliary equipment
Configure the line for the market you sell into. Popular additions include:
- Gravimetric dosing and masterbatch colour unit
- Additional die heads and calibrators for new microduct sizes
- Online diameter, ovality and wall thickness measurement
- Double-station winder and automatic coil handling
- Coil packing and film wrapping machine
- Remote control and production data logging
Why buy from BENK Machinery
Extrusion specialists, not traders
BENK designs and builds extrusion lines in Zhangjiagang with an in-house R&D and process team, so machine selection is matched to your resin and product instead of a catalogue number.
Evidence before shipment
Every line is assembled and run in our works. You receive trial video, diameter and output records, and are welcome to attend the factory acceptance test.
Total cost, not lowest price
Energy-efficient drives, permanent magnet motors and optimized heating reduce kWh per tonne, which usually matters more over five years than the initial purchase price.
Real commissioning support
Our engineers install, commission, train your operators and stay involved until the line hits the specified output and quality on your material.
Spares and response
Critical spares are stocked for fast dispatch, and the Siemens Ethernet control platform allows remote diagnostics and software updates.
Upgrades as you grow
Additional die heads, calibrators, co-extruders and winders can be added later, so the line grows with the duct sizes and bundle types you sell.
Frequently asked questions
The questions buyers ask most often about this line.
What is the difference between a smooth-wall and a ribbed-wall microduct?
Which sizes are covered?
How is the production speed set?
Is the silicone layer on the ribbed duct the same as on a smooth duct?
What is included in the delivery?
Get a quotation for the Ribbed-wall Silicon-core Microduct Production Line
Tell us the duct sizes or bundle types, the raw material, the target line speed and the country the line will be installed in. We will reply with a sized configuration, a budgetary price and an indicative delivery time.
- Telephone
- +86 512 5896 1463
- Mobile / WhatsApp / WeChat
- +86 159 5096 2426
- kpm@benkpm.com
- Address
- No.20 Huatang Road, Economic Development Zone (South District), Zhangjiagang City, Jiangsu, China
Related extrusion lines
Zhangjiagang City BENK Machinery Co., Ltd. · www.benkpm.com · Plastic extrusion lines and extruders since 2004.