Case Studies & Project References
Selected projects delivered by BENK Machinery -from single extrusion lines to complete turnkey projects with documentation, CE certification, third-party validation and factory acceptance testing (FAT).
 AUTOMOTIVE · FRANCE · 2026
FORVIA Group -PP Retainer Profile Extrusion Line
| Customer | FORVIA Group (French automotive Tier-1 supplier) |
|---|---|
| Location | France |
| Material / product | PP -retainer profile |
| Scope of supply | Complete extrusion line + critical spare parts list |
| Technical documentation | Preventive maintenance manual, instruction manual, full line documentation package |
| Project planning | Transportation lead time and cost, installation & setup, maintenance and service, process support |
| Compliance | CE certification, third-party validation according to safety and regulation |
| Acceptance | FAT (Factory Acceptance Test) title presentation -2026 |
Automotive work leaves little room for improvisation. Before the line was built, FORVIA received a quotation broken down line by line, with the critical spare parts listed separately, so the purchasing team could see exactly what a year of operation would need.
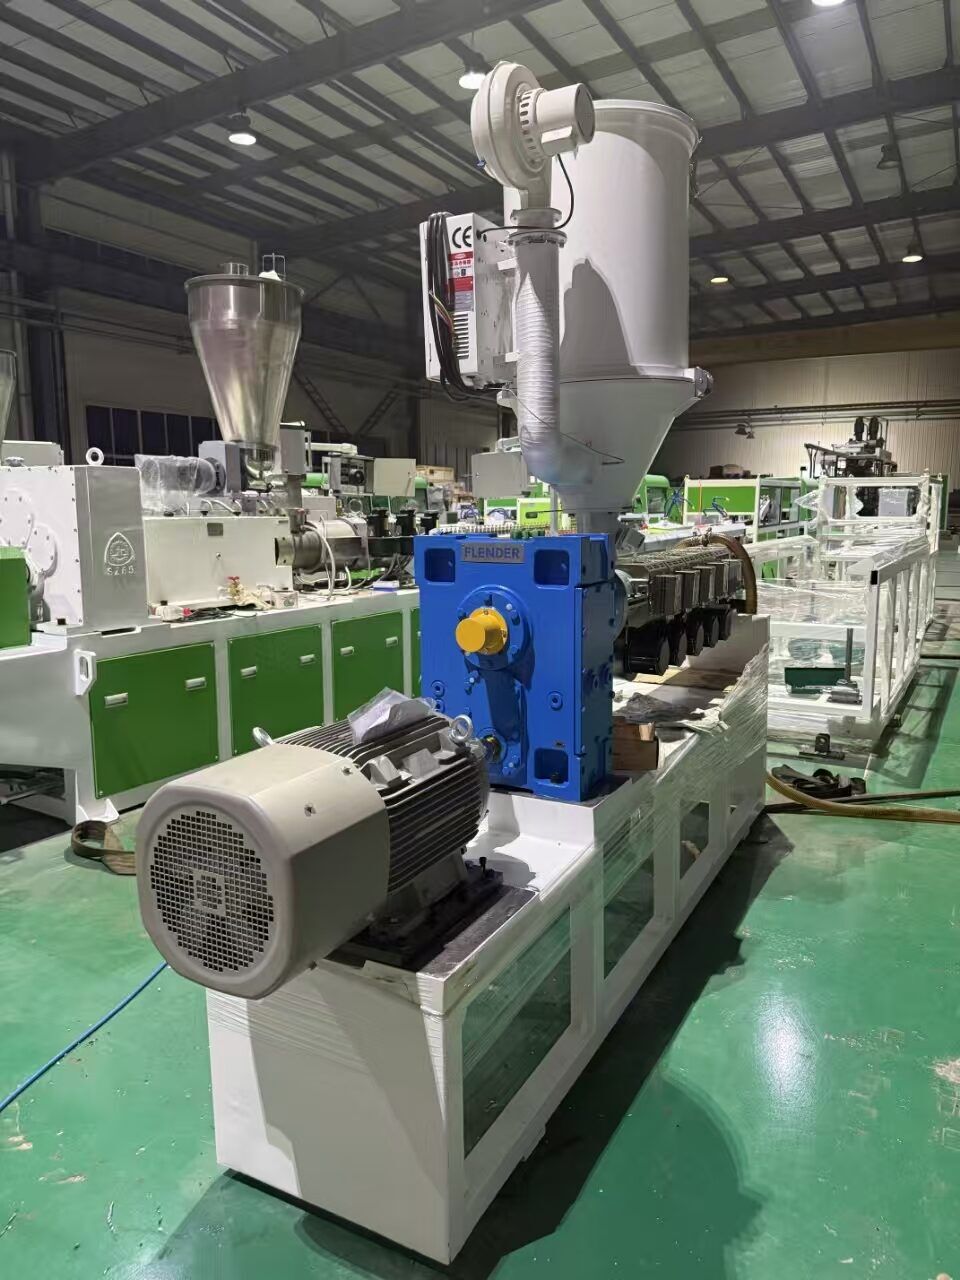
On the technical side the package included the maintenance and instruction manuals, the safety and regulation documents and the CE certification file. A third party reviewed the safety functions, and the retainer profile extrusion line ran through a full factory acceptance test at our workshop before it was packed for France.
Customer visit & acceptance
Workshop test run before shipment
Short clip from the workshop test run — retainer profile line running before packing.
PET Sheet Production Line -FAT & Electrical Assembly
| Product | PET sheet production line |
|---|---|
| Location | Poland |
| Capacity | 850 kg/h |
| Sheet width | 800 mm |
| Delivery | 2025 |
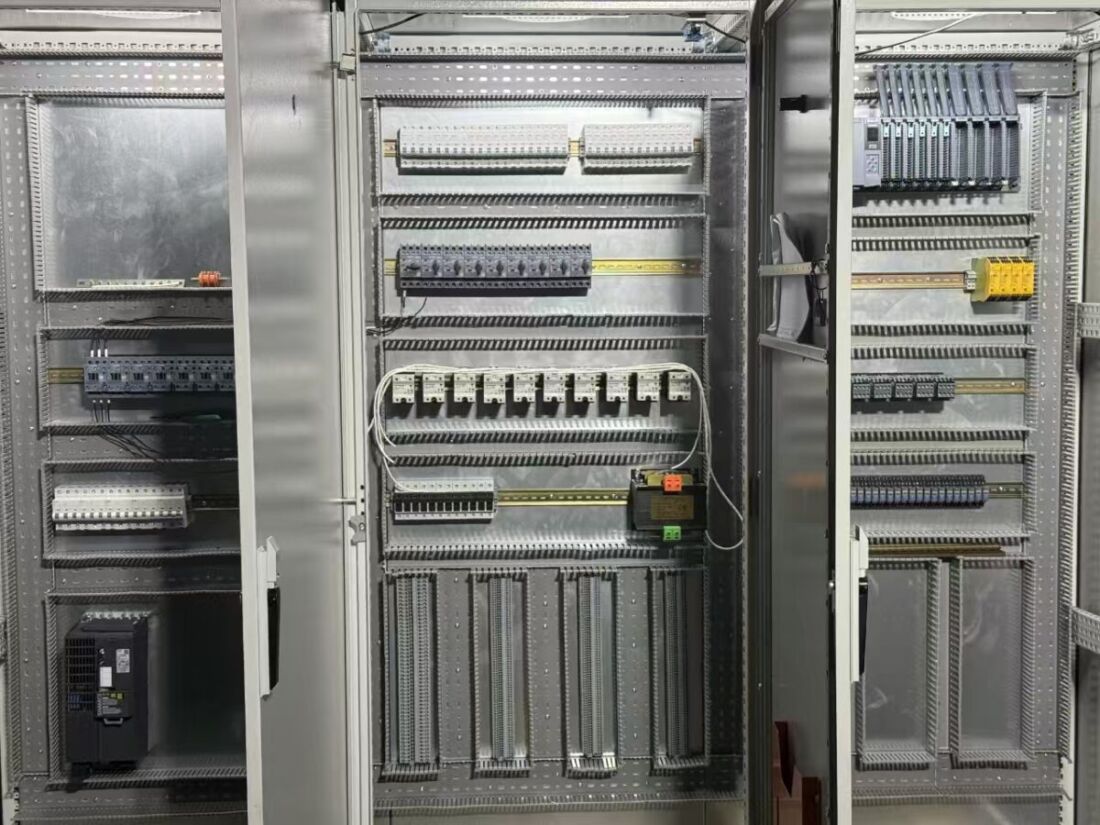
| Project stage | Electrical assembly, control cabinet wiring and pre-delivery testing |
| Included in scope | Control cabinets, drive and PLC panels, safety circuitry, full wiring documentation |
| Verification | Bench testing before shipment (FAT) |
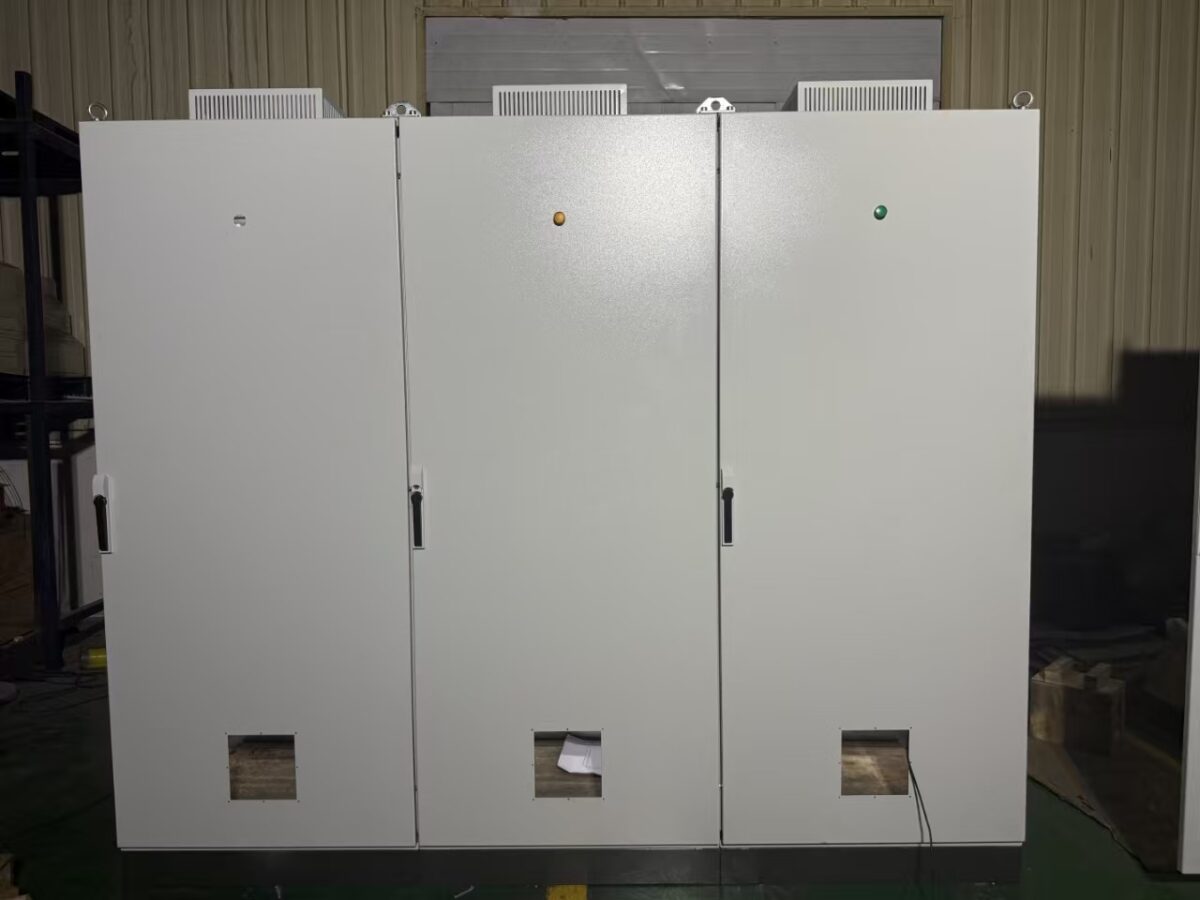
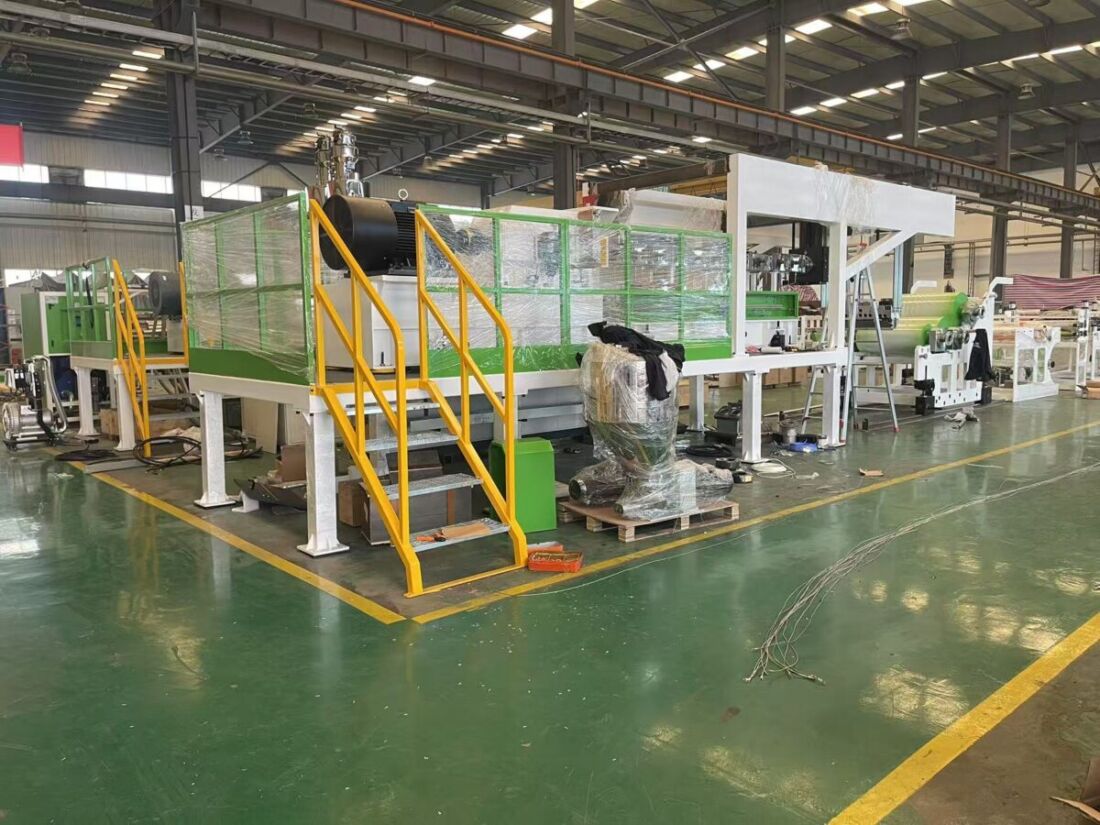
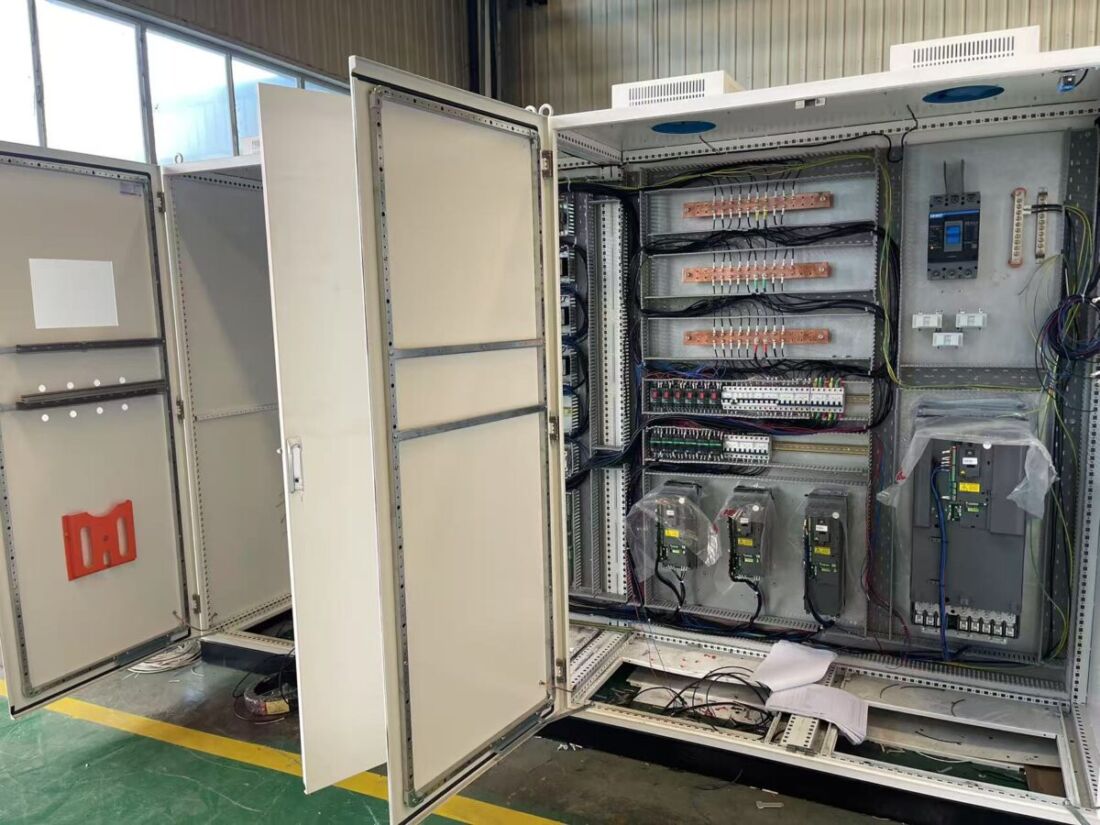
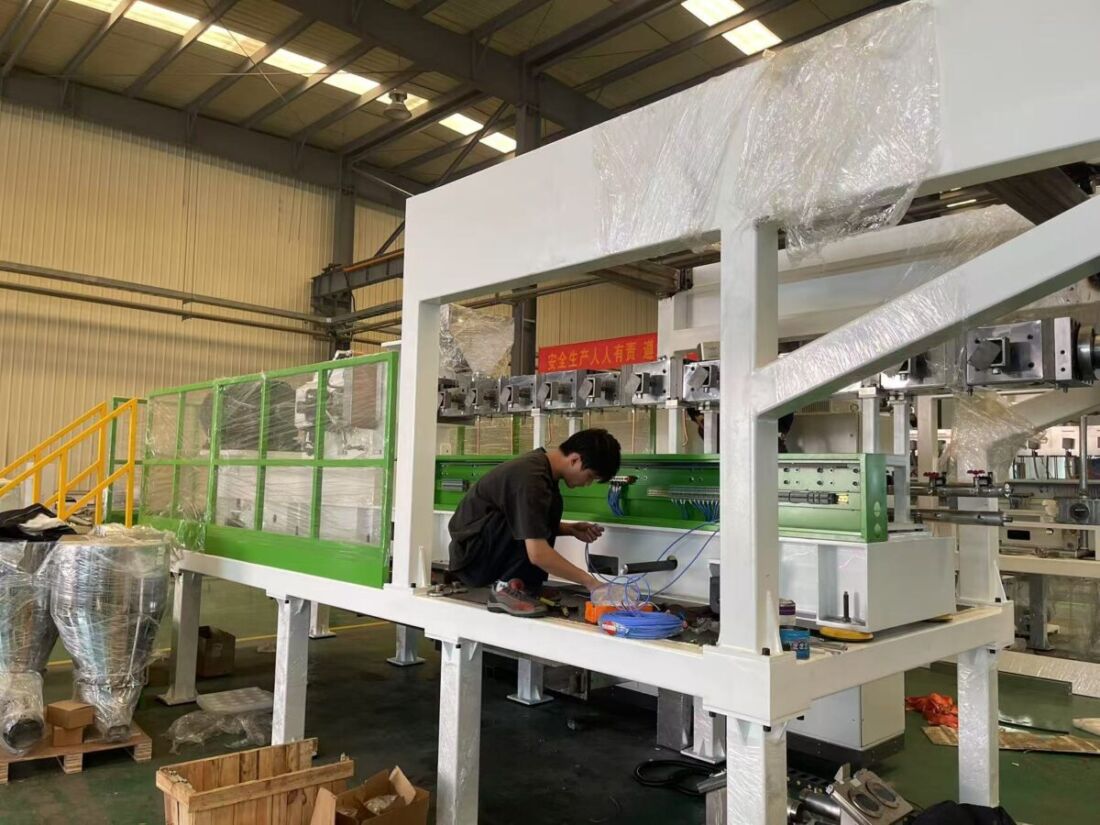
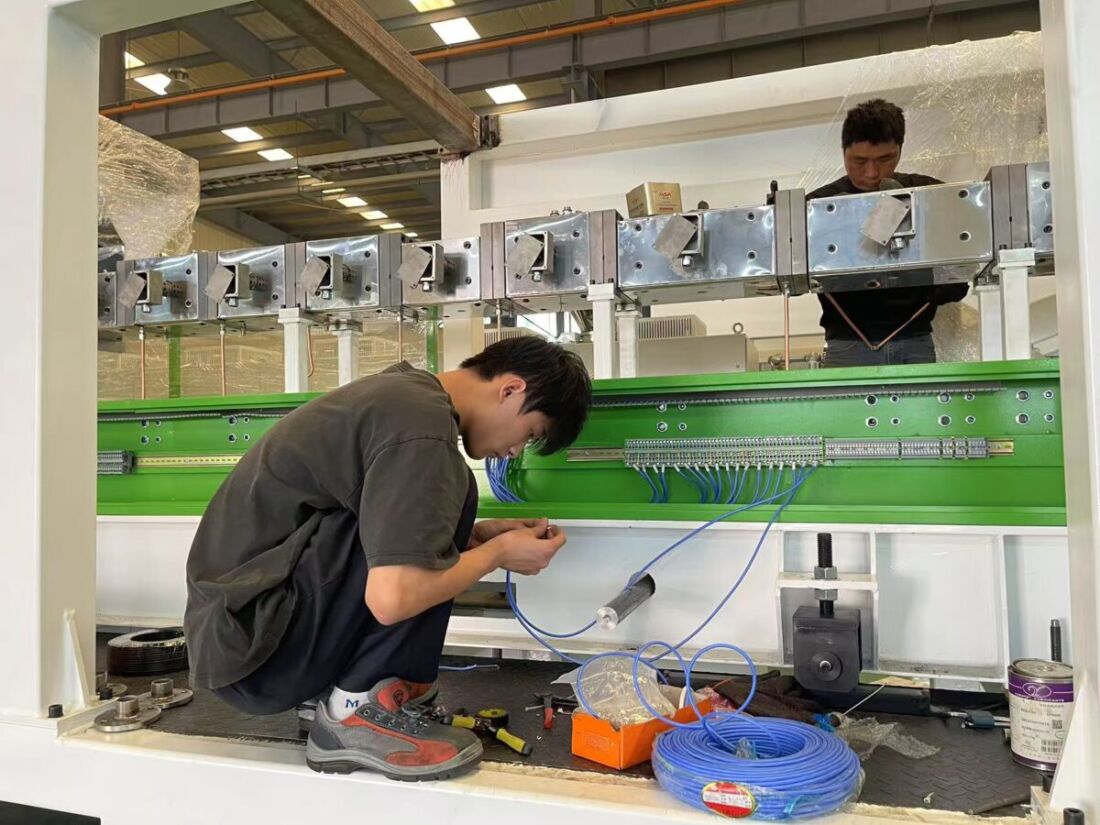
The panels for this PET sheet extrusion line were built and tested before the mechanical assembly was finished. Every circuit is wired to drawing and labelled, each drive and safety component is checked on its own, and the complete set is re-tested with the line running at our workshop.
Wiring is the part buyers rarely see on a quotation, but it decides how quickly a thermoforming sheet line can be commissioned on site. Because the cabinets arrive documented and tested, the installation team starts from a working control system instead of a box of loose wires.
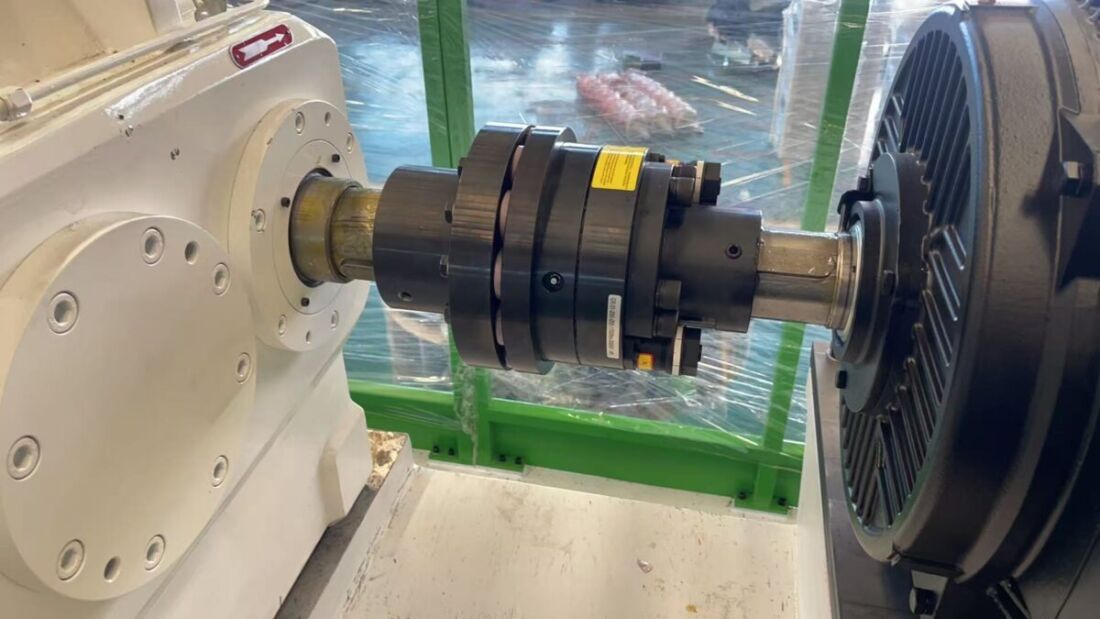
CONSUPLAST — 63-160 mm PVC Double Cavity Pipe Production Line
| Customer | CONSUPLAST (Ecuador) — one of the leading plastic processing companies in Ecuador |
|---|---|
| Location | Ecuador |
| Product | PVC pipe production line, double cavity (two pipes per die) for 63-160 mm PVC pipe |
| Extruder | Counter-rotating parallel twin screw extruder (异向平双) — PVC powder direct extrusion |
| Scope of supply | Complete PVC pipe extrusion line: extruder, twin die head, vacuum calibration tanks, haul-off, cutting machine, stacking |
| Applications | Water supply, irrigation and drainage pipe for the Andean and Latin American market |
| Documentation | Operation manual, maintenance manual, layout drawing and spare-part list |
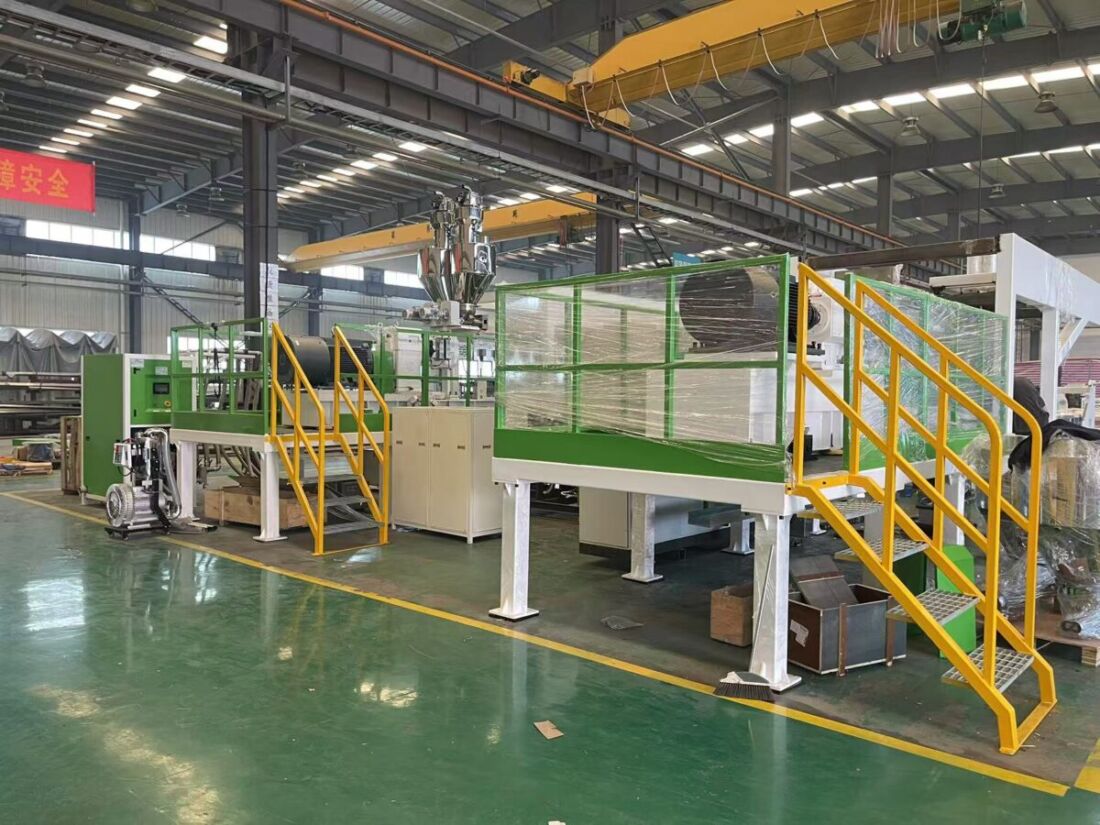
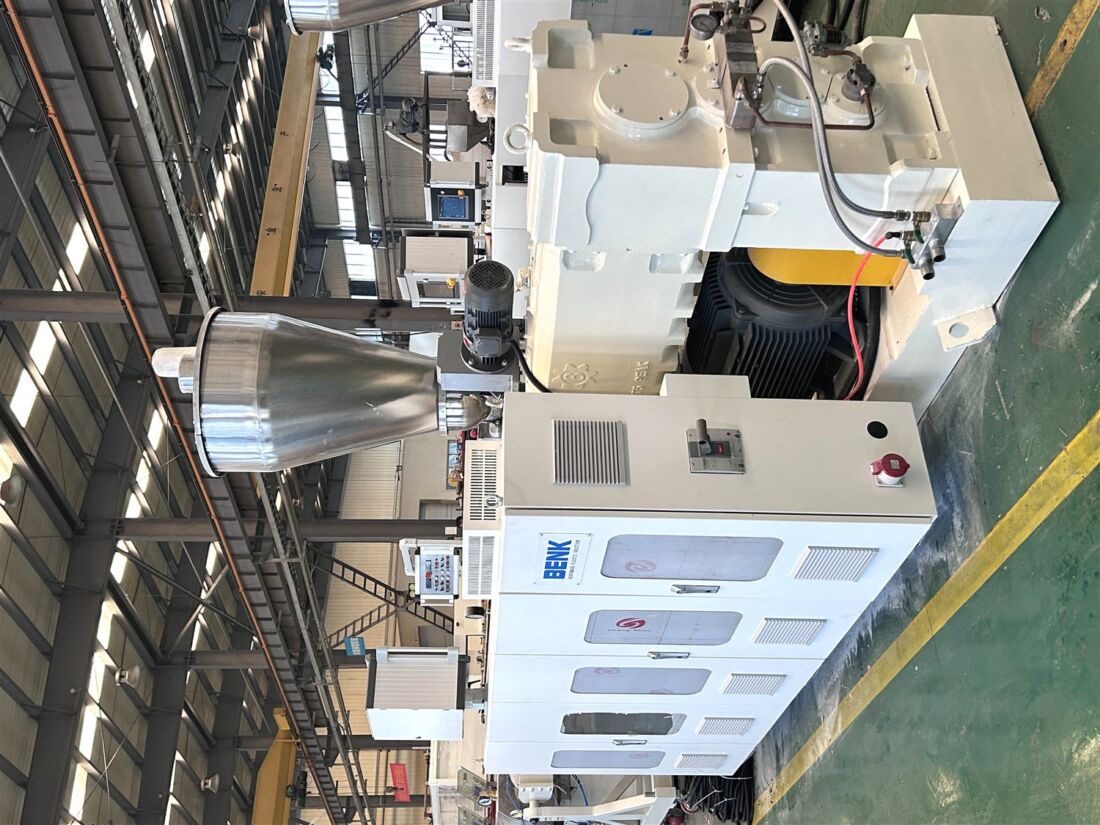
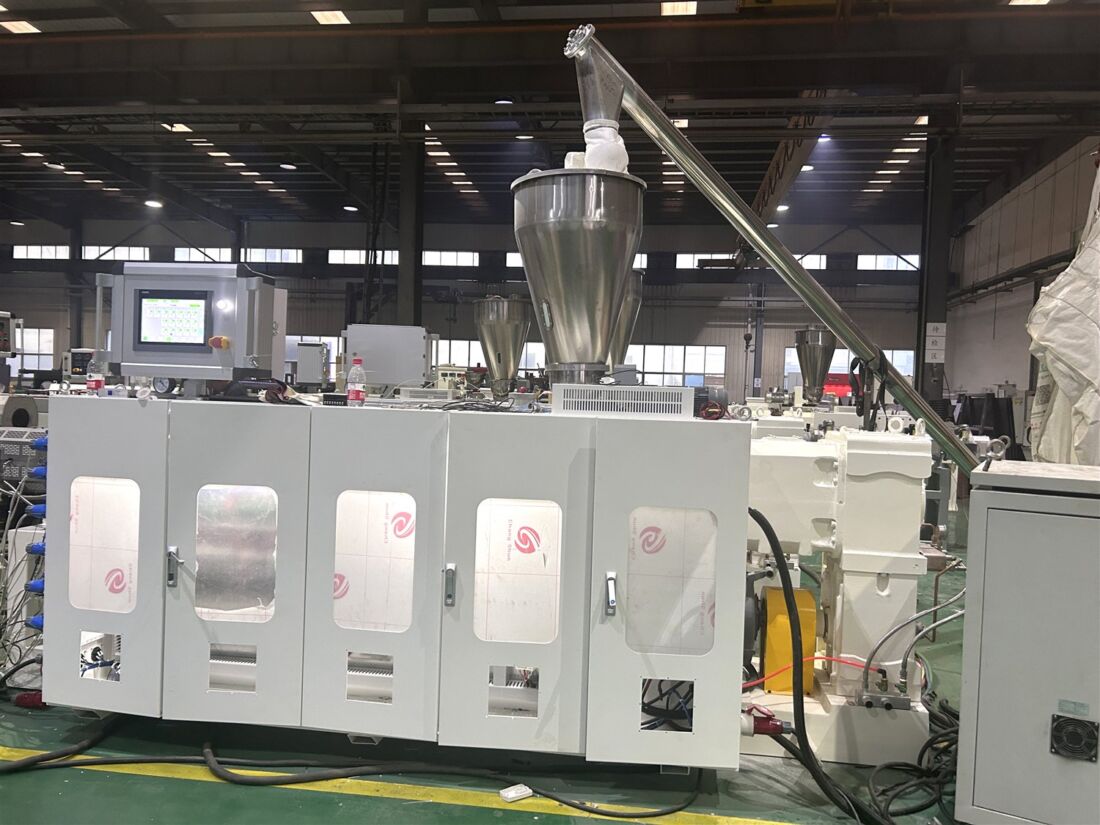
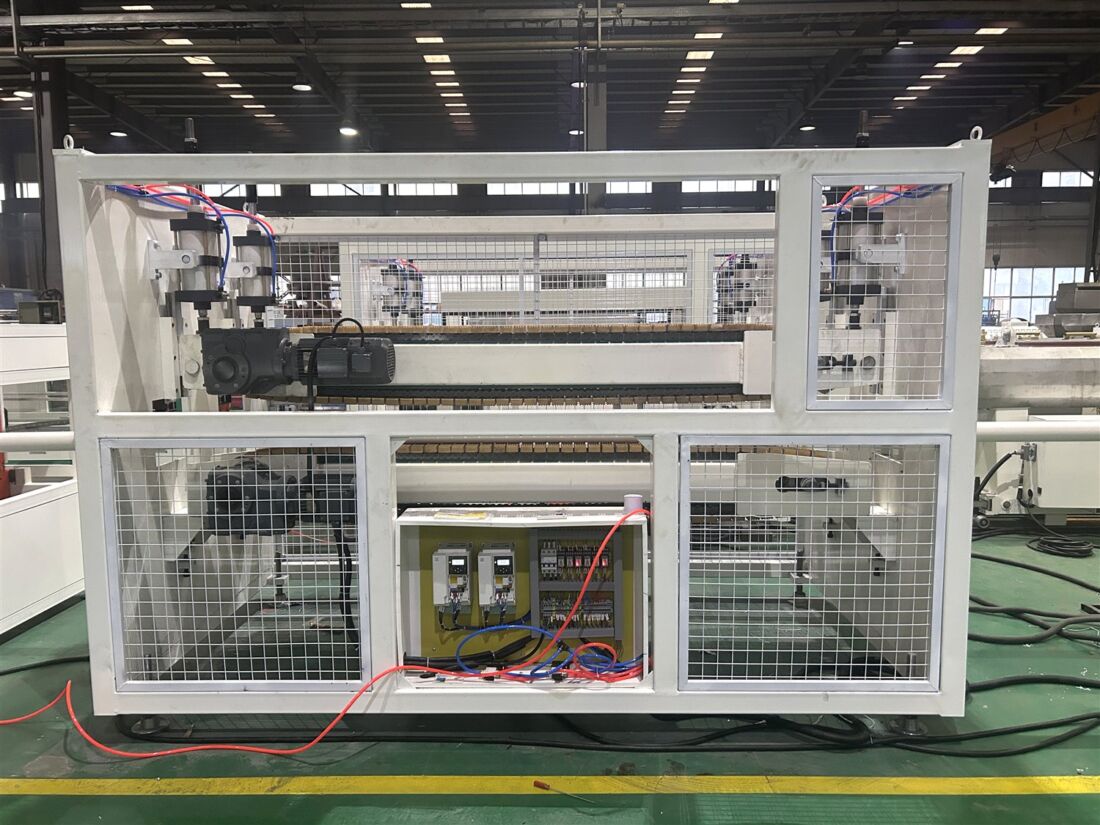
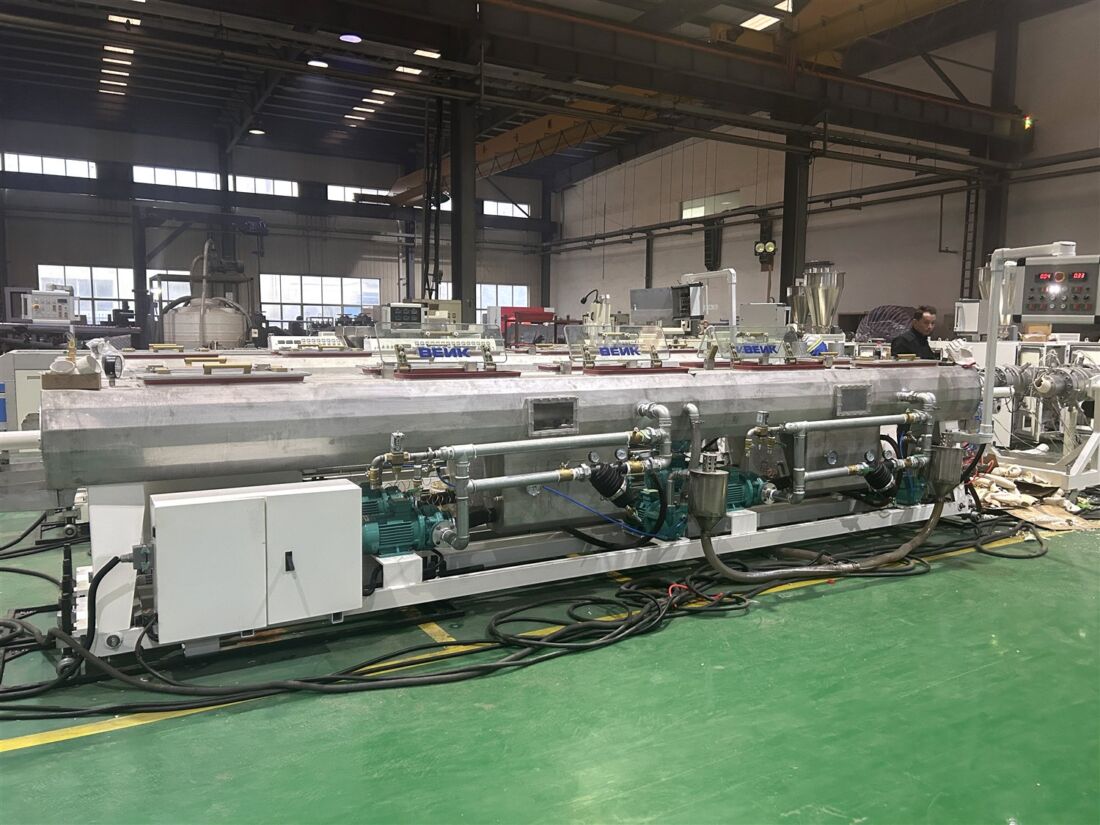
CONSUPLAST runs some of the busiest PVC extrusion capacity in Ecuador, and they came to us for a line that could raise output without a second extruder. The answer was a double cavity set-up: one counter-rotating parallel twin screw extruder feeding a twin die head, producing two 63-160 mm PVC pipes at the same time.
A double cavity PVC pipe production line is more than a two-hole die. Both cavities have to be fed evenly, otherwise one pipe runs thick and the other thin. We matched the die head, the vacuum calibration tanks and the two-track haul-off so wall thickness and roundness stay inside tolerance on both pipes at the same haul-off speed. On the same floor space, with one operator and one set of downstream equipment, that is close to twice the output of a single cavity PVC pipe machine.
BENK supplies complete PVC pipe making machines, double cavity pipe extrusion lines and counter-rotating parallel twin screw extruders for PVC, CPVC, UPVC and PE applications, with factory acceptance testing before shipment and overseas installation and training.
Leading US PVC pipe manufacturer — 16-32 mm PVC Four Cavity Pipe Production Line
| Customer | One of the leading PVC pipe manufacturers in the United States (customer name available on request) |
|---|---|
| Location | United States |
| Product | PVC pipe production line, four cavity (four pipes per die head) for 16-32 mm PVC pipe |
| Extruder | Counter-rotating parallel twin screw extruder — PVC powder direct extrusion |
| Scope of supply | Complete line: parallel twin screw extruder, four cavity die head, vacuum calibration and cooling tanks, four-track haul-off, cutting unit and automatic belling machine |
| Key feature | Four pipes produced simultaneously from one extruder — roughly 3-4x the output of a single cavity PVC pipe machine at the same screw diameter |
| Documentation | Operation manual, maintenance manual, layout drawing, spare-part list and factory acceptance test |
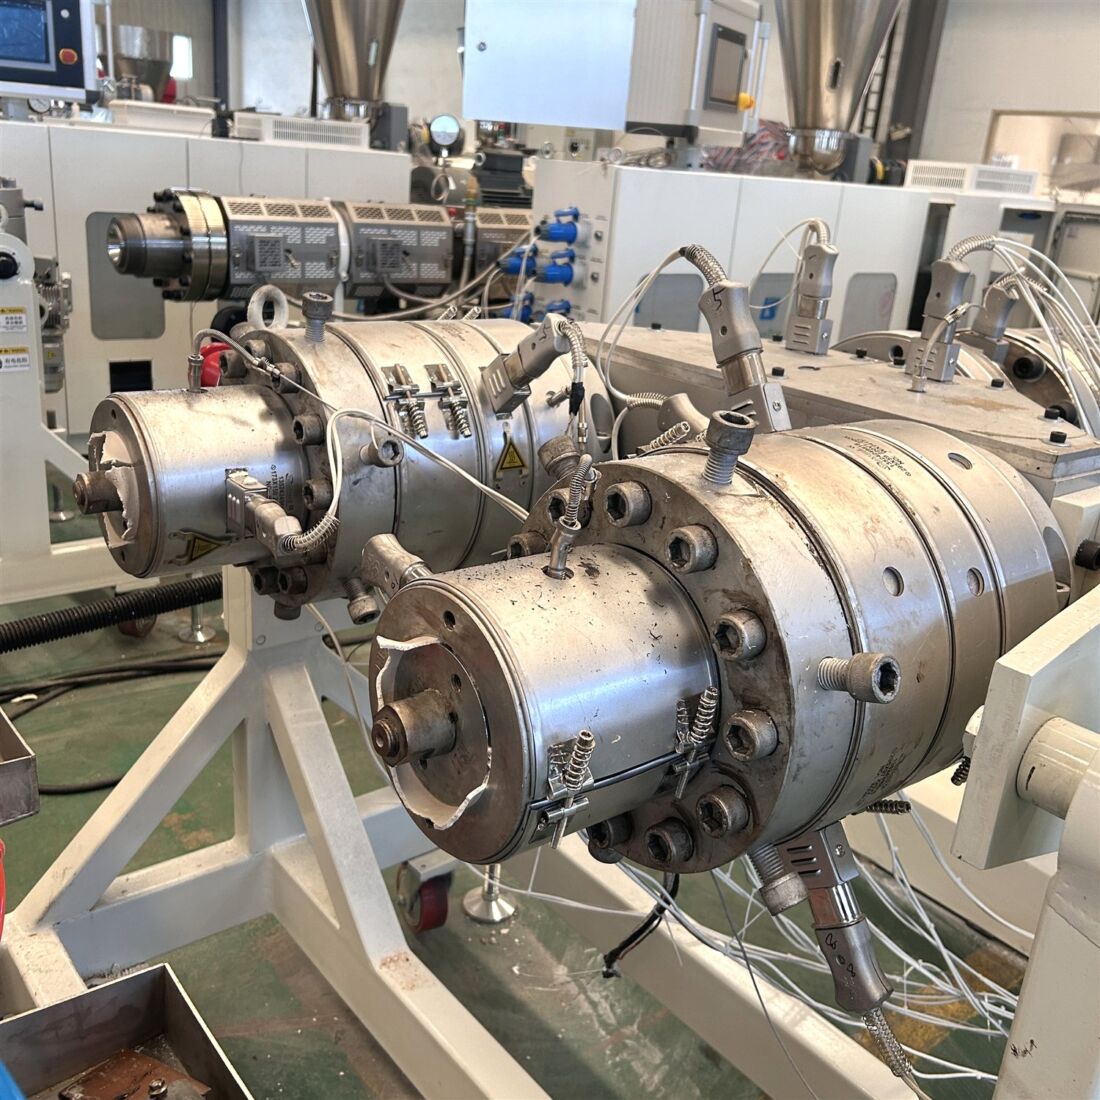
For this American customer the requirement was simple to state and hard to build: 16-32 mm pipe, in volume, without adding extruders. Four cavity extrusion is the economical answer at that diameter. One counter-rotating parallel twin screw extruder feeds a four cavity die head, and four pipes leave the die together.
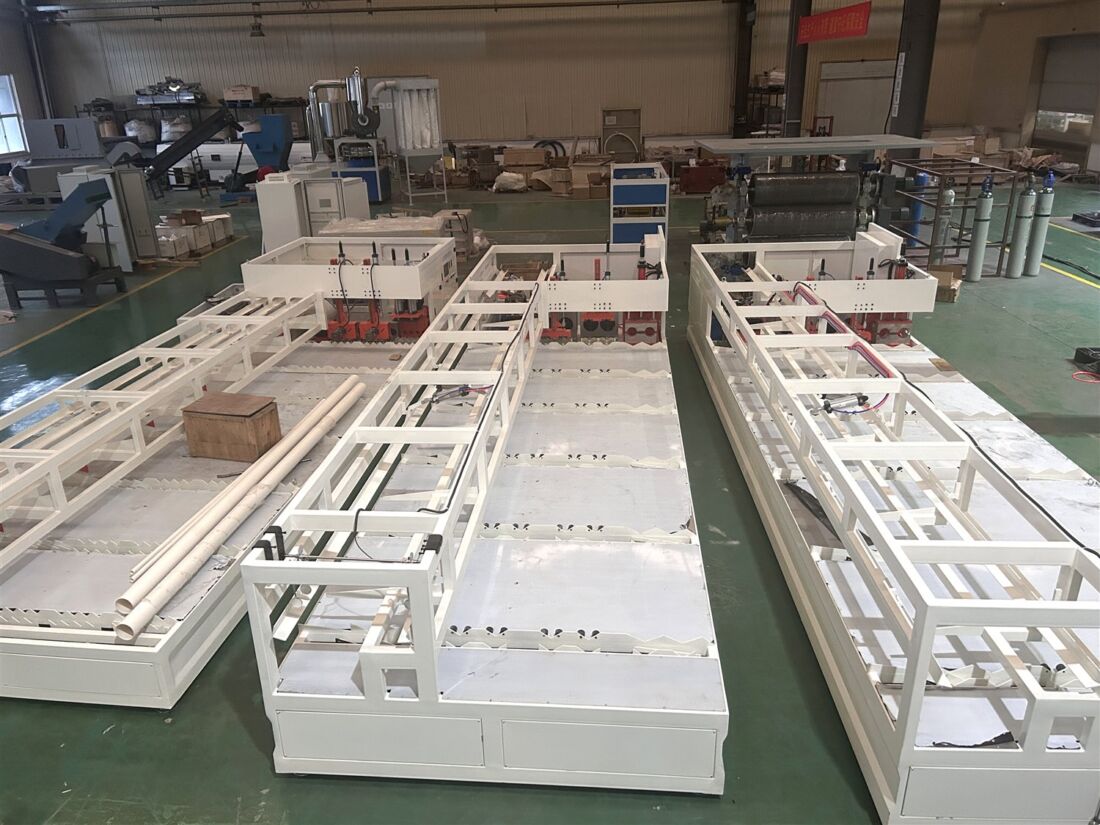
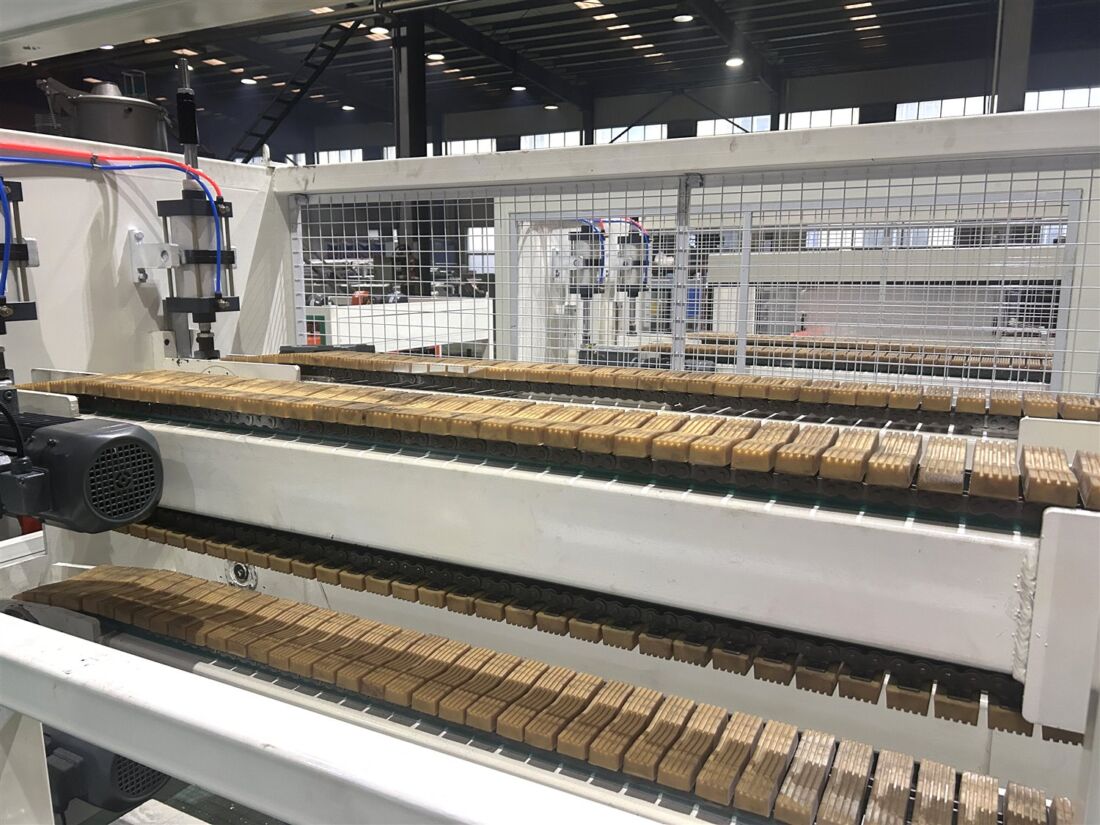
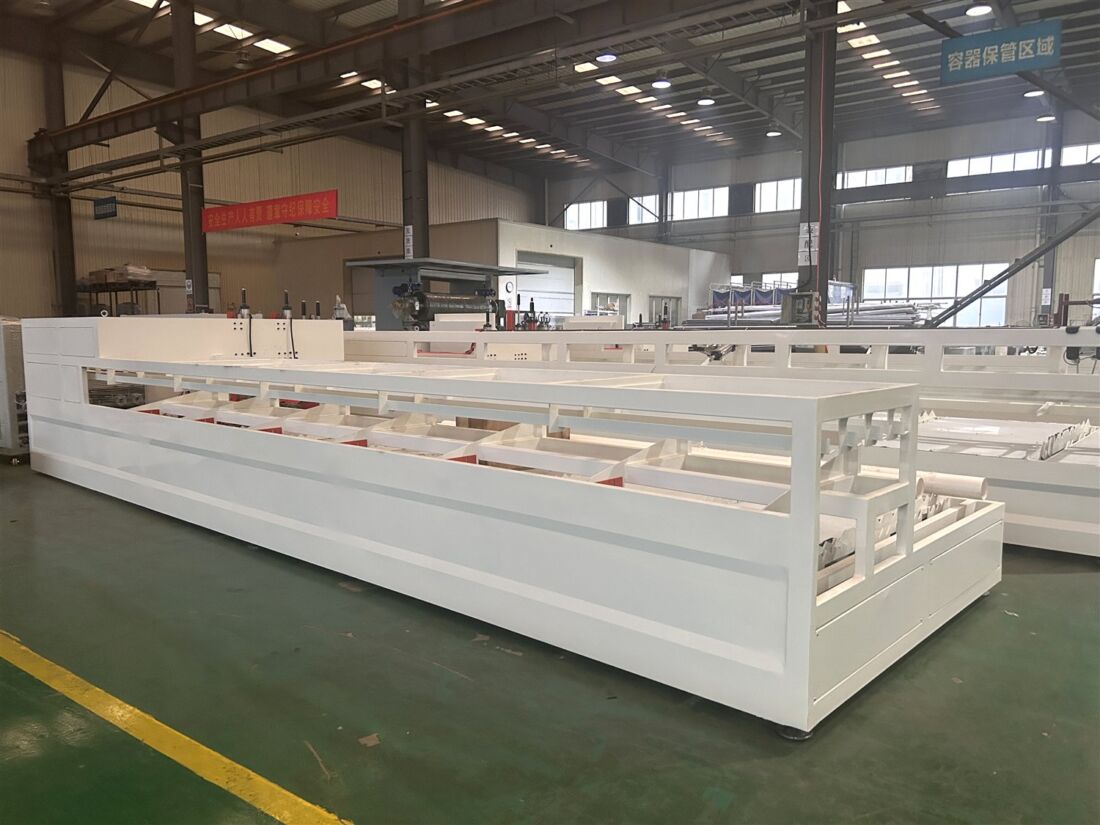
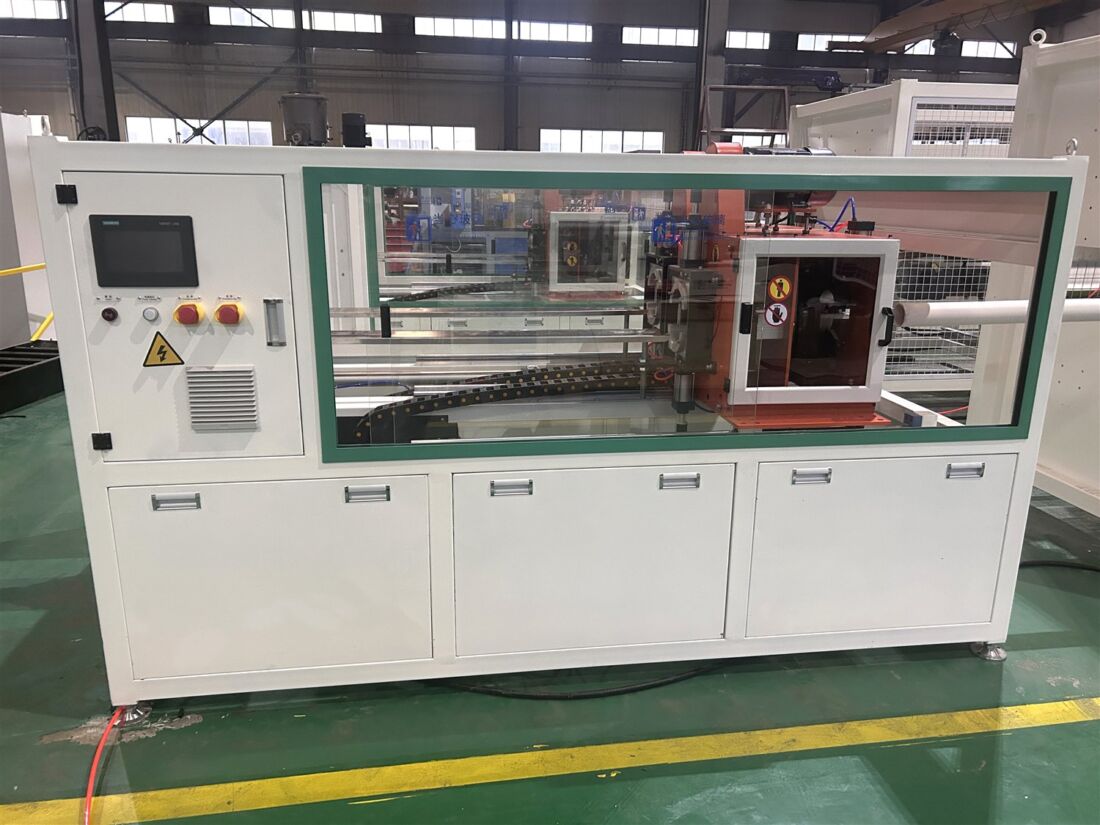
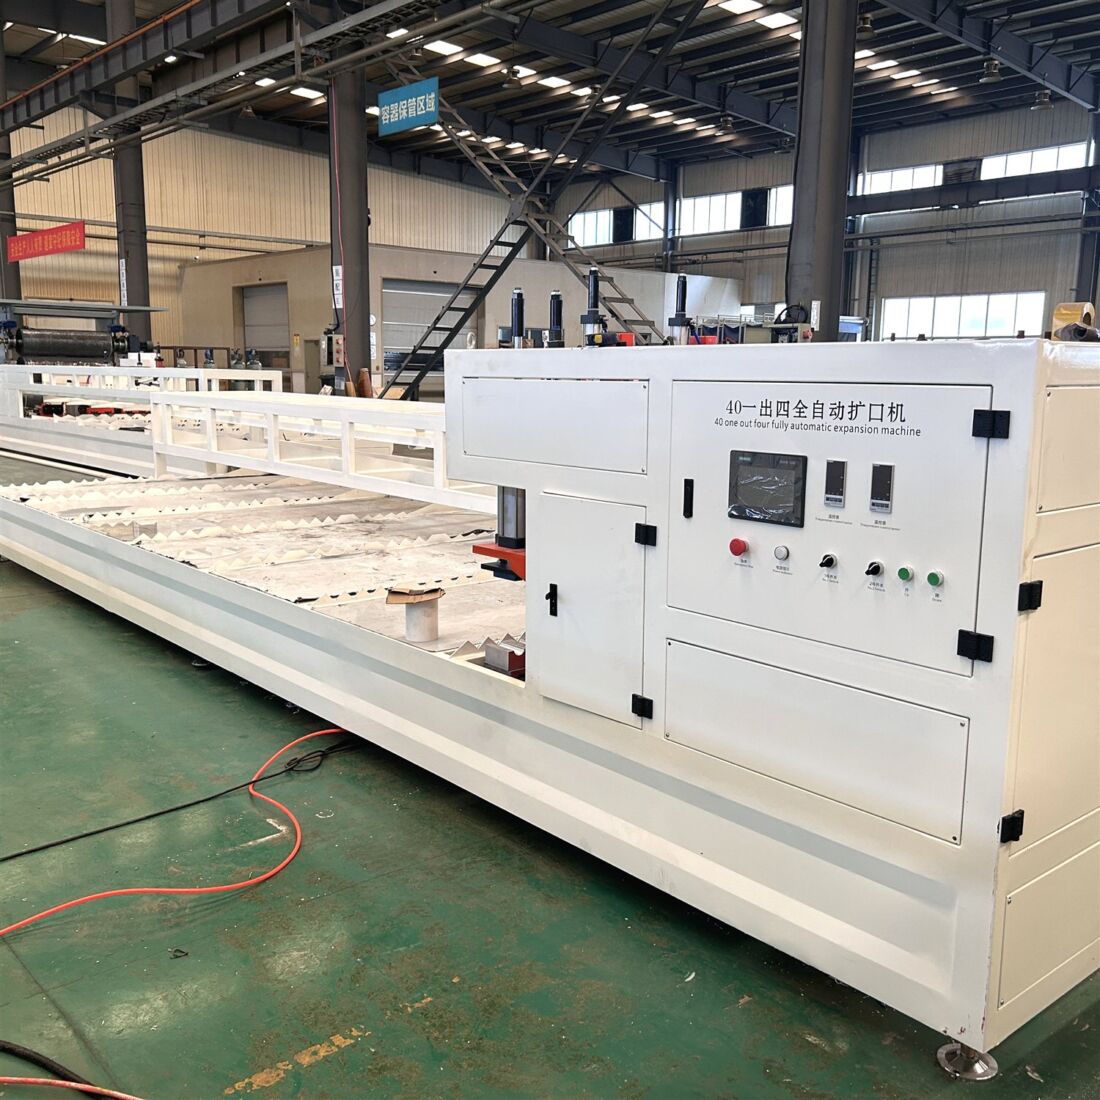
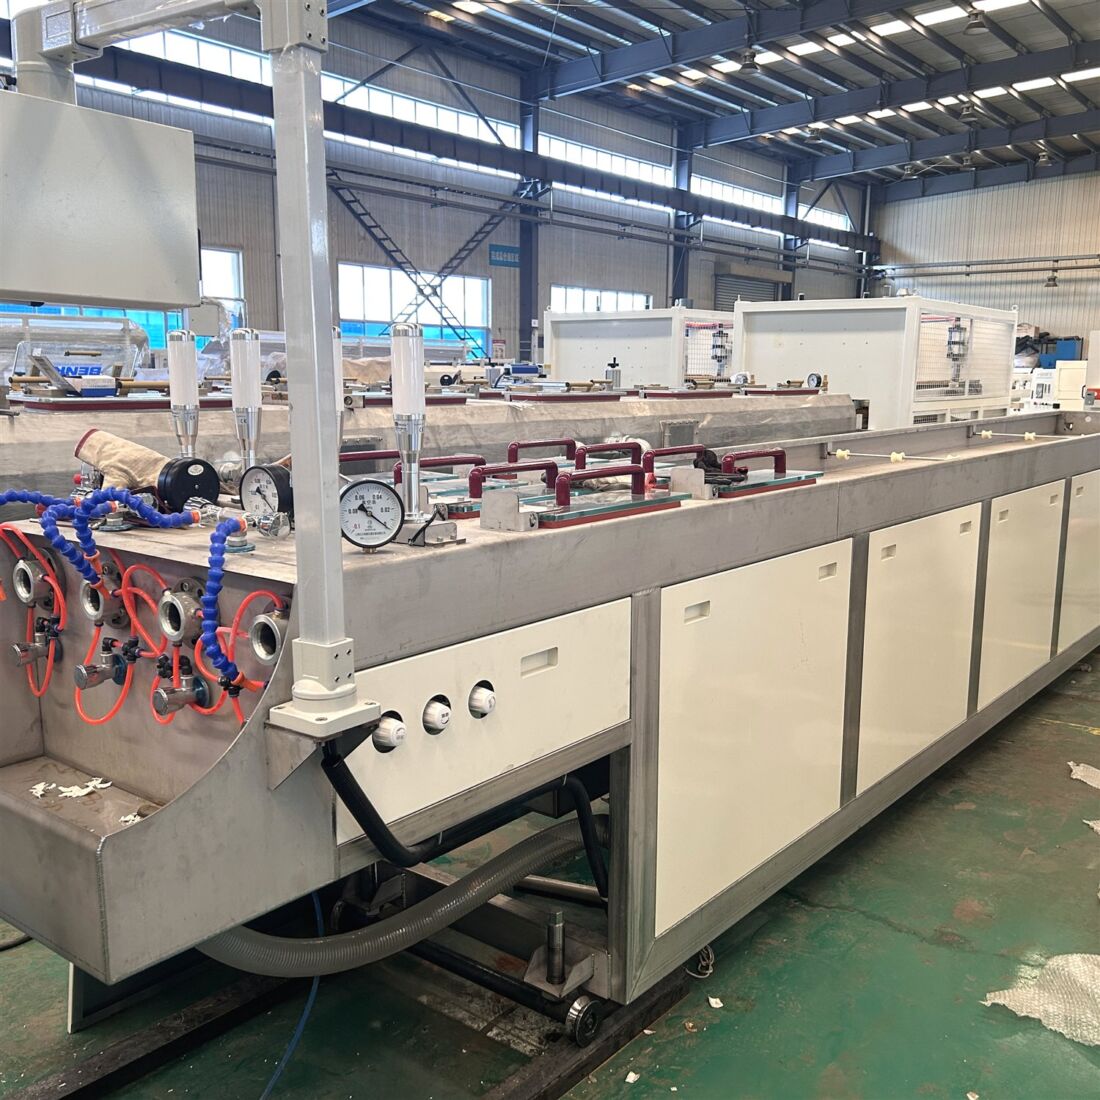
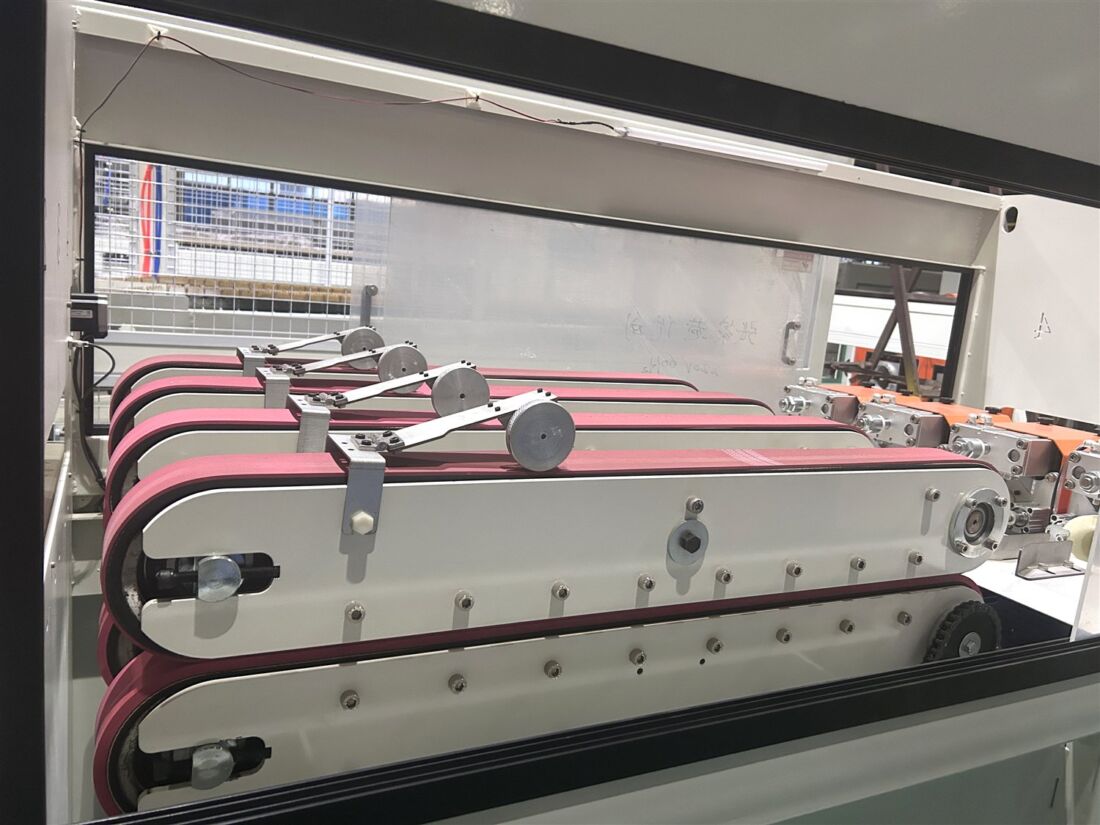
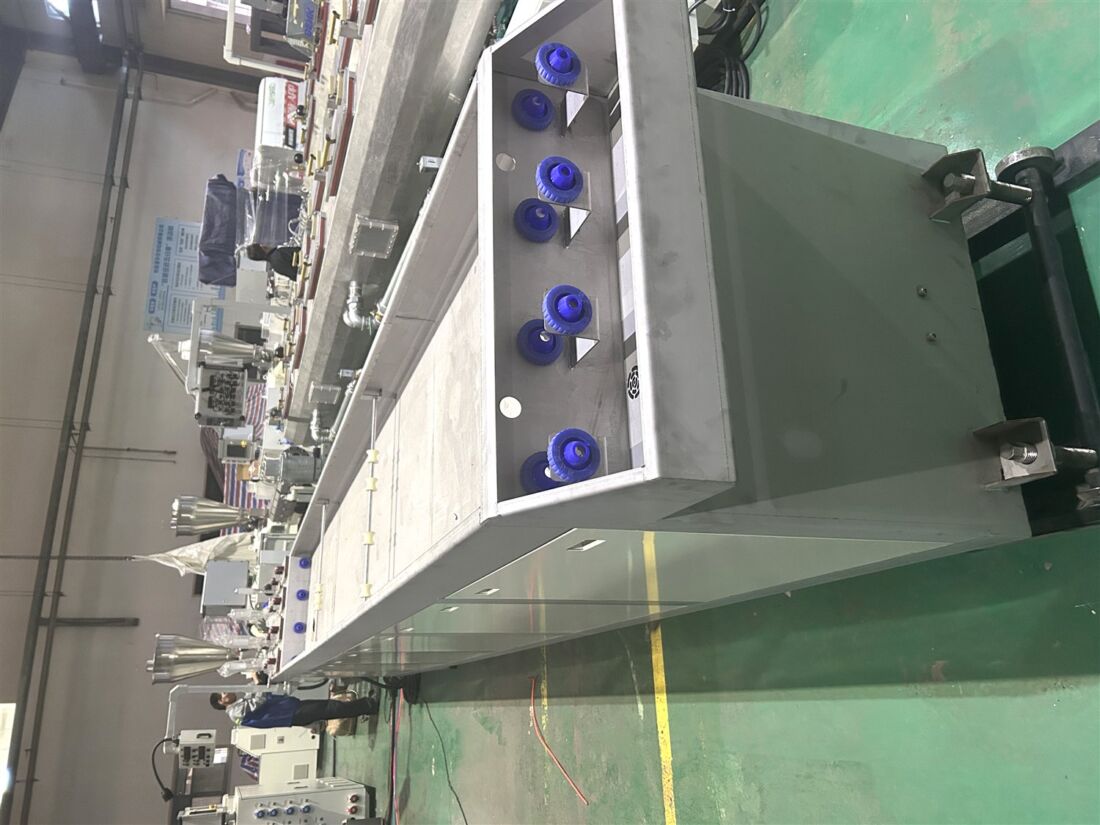
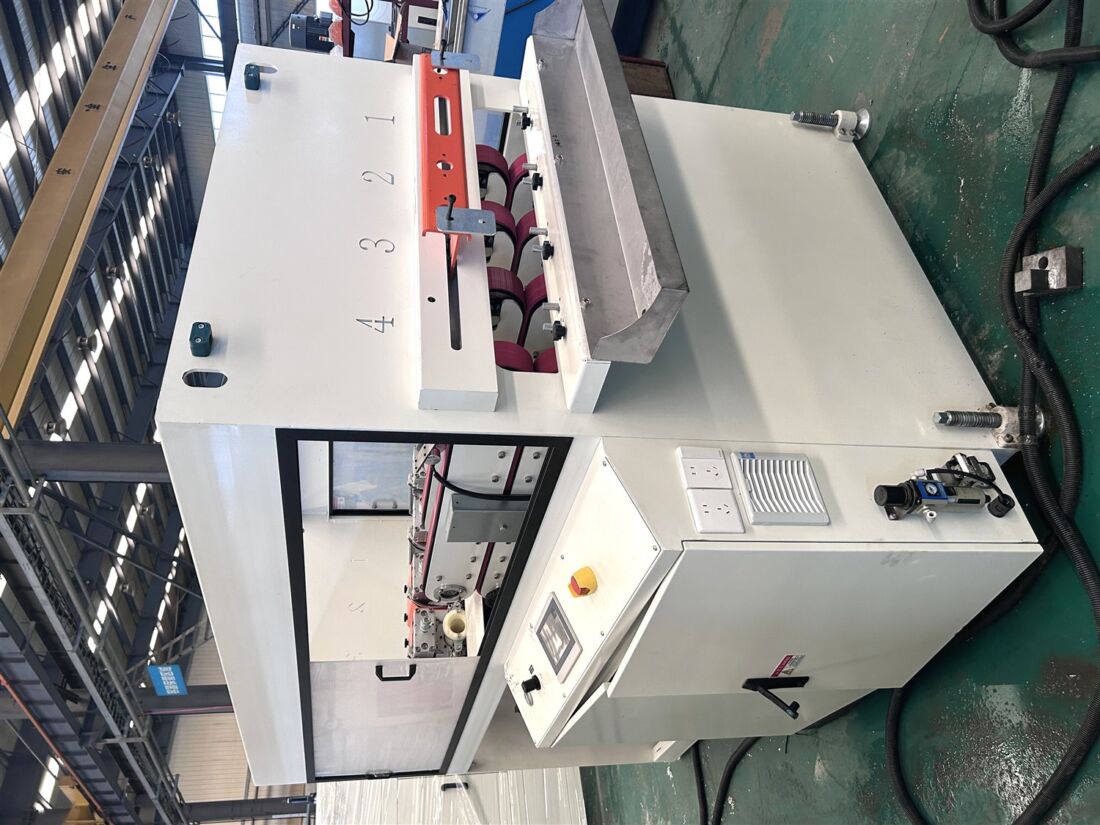
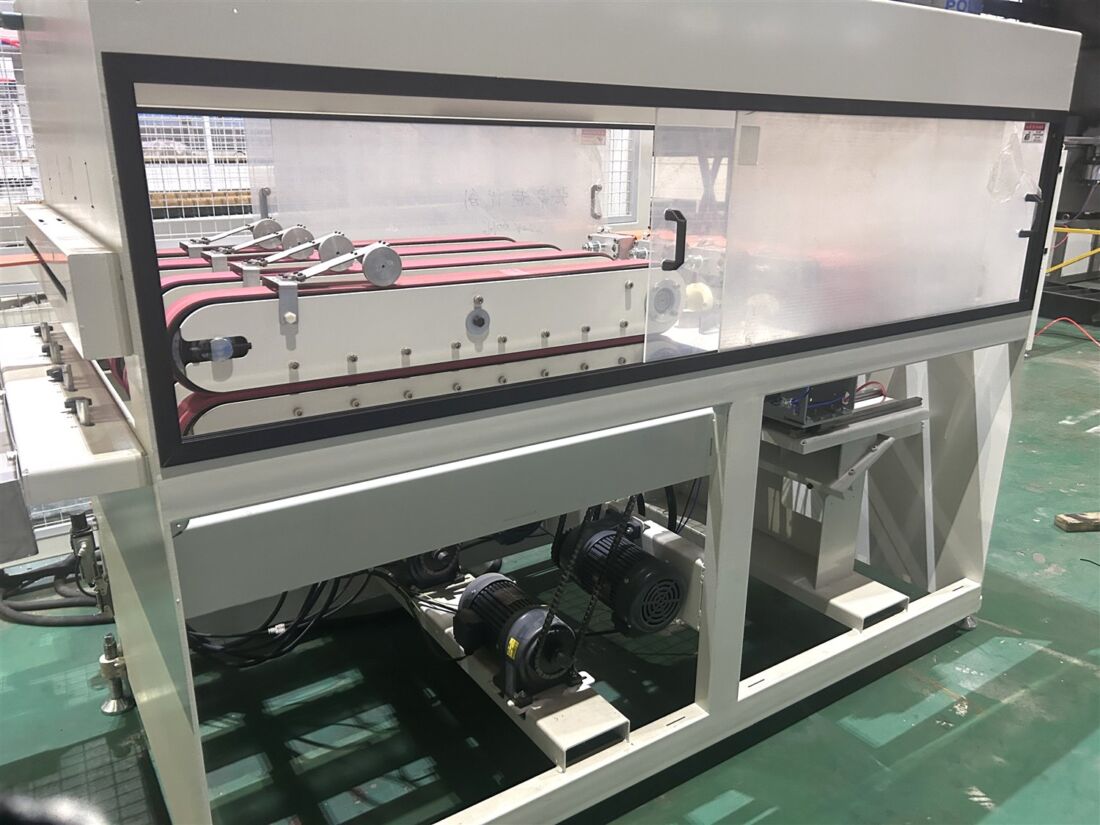
Keeping the four cavities balanced is most of the engineering. The die is flow-designed so each cavity sees the same pressure, the vacuum calibration tank is divided into four tracks with individual sizing sleeves, and the haul-off drives four synchronised belts so no pipe is pulled faster than its neighbours. Downstream the line cuts to length and bells automatically; the unit in these photos is a 40 mm one-out-four fully automatic belling machine.
A four cavity PVC pipe line only pays off if it stays running, so cooling length, belt wear and changeover time are designed in from the start rather than added later.
BENK builds complete PVC pipe making machines, multi cavity pipe extrusion lines (double cavity and four cavity) and counter-rotating parallel twin screw extruders, together with automatic PVC pipe belling machines. Lines are assembled and factory-tested in our workshop, then shipped with full documentation and overseas installation support.
Samsung Group subsidiary (Korea) — 160-450 mm PVC Pipe Production Line
| Customer | A subsidiary of the Samsung Group in South Korea, one of the country’s leading industrial groups (customer name available on request) |
|---|---|
| Location | South Korea |
| Product | PVC pipe production line for 160-450 mm pipe (large diameter), single pipe per die |
| Extruder | Extruder sized for the 160-450 mm pipe range, model confirmed per project and pipe schedule |
| Scope of supply | Complete line: extruder, die head and sizing, vacuum calibration tank, spray cooling tank, multi-belt haul-off, cutting unit and belling |
| Key point | Large diameter pipe needs long, temperature-stable calibration and cooling; the tank length and spray zones in this line were sized for 450 mm wall thicknesses |
| Documentation | Operation manual, maintenance manual, layout drawing, spare-part list and factory acceptance test |
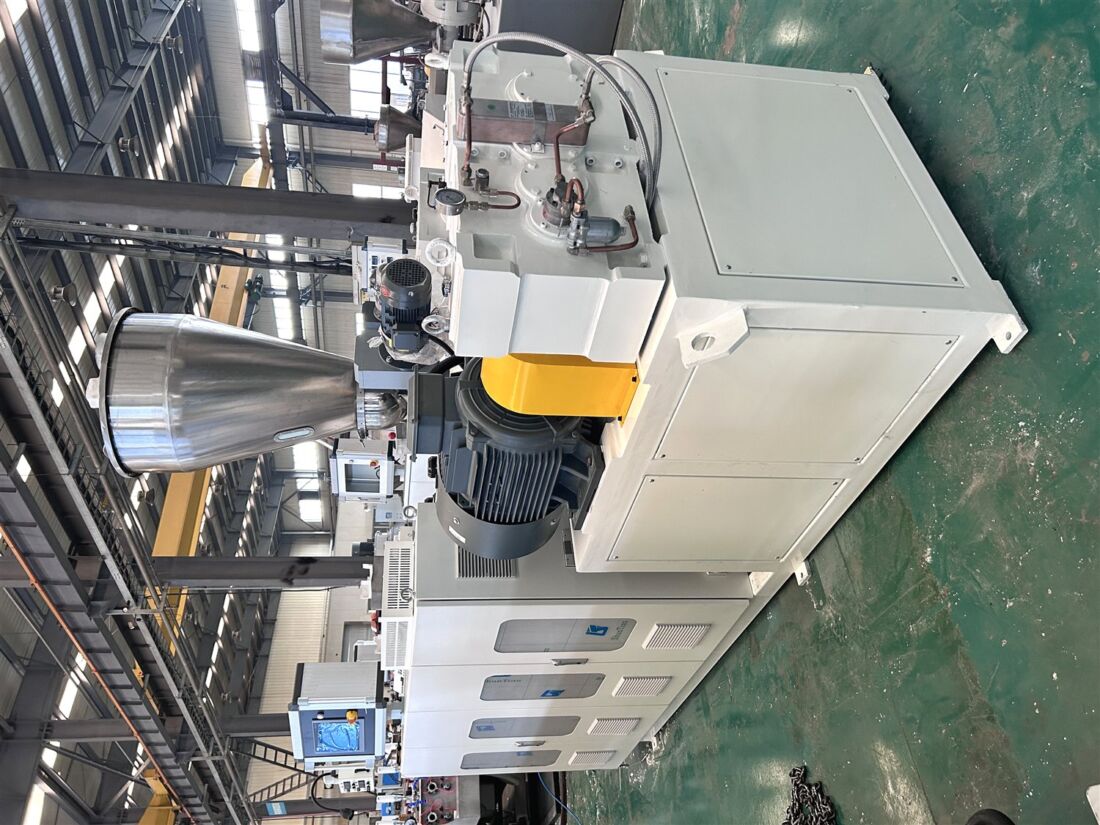
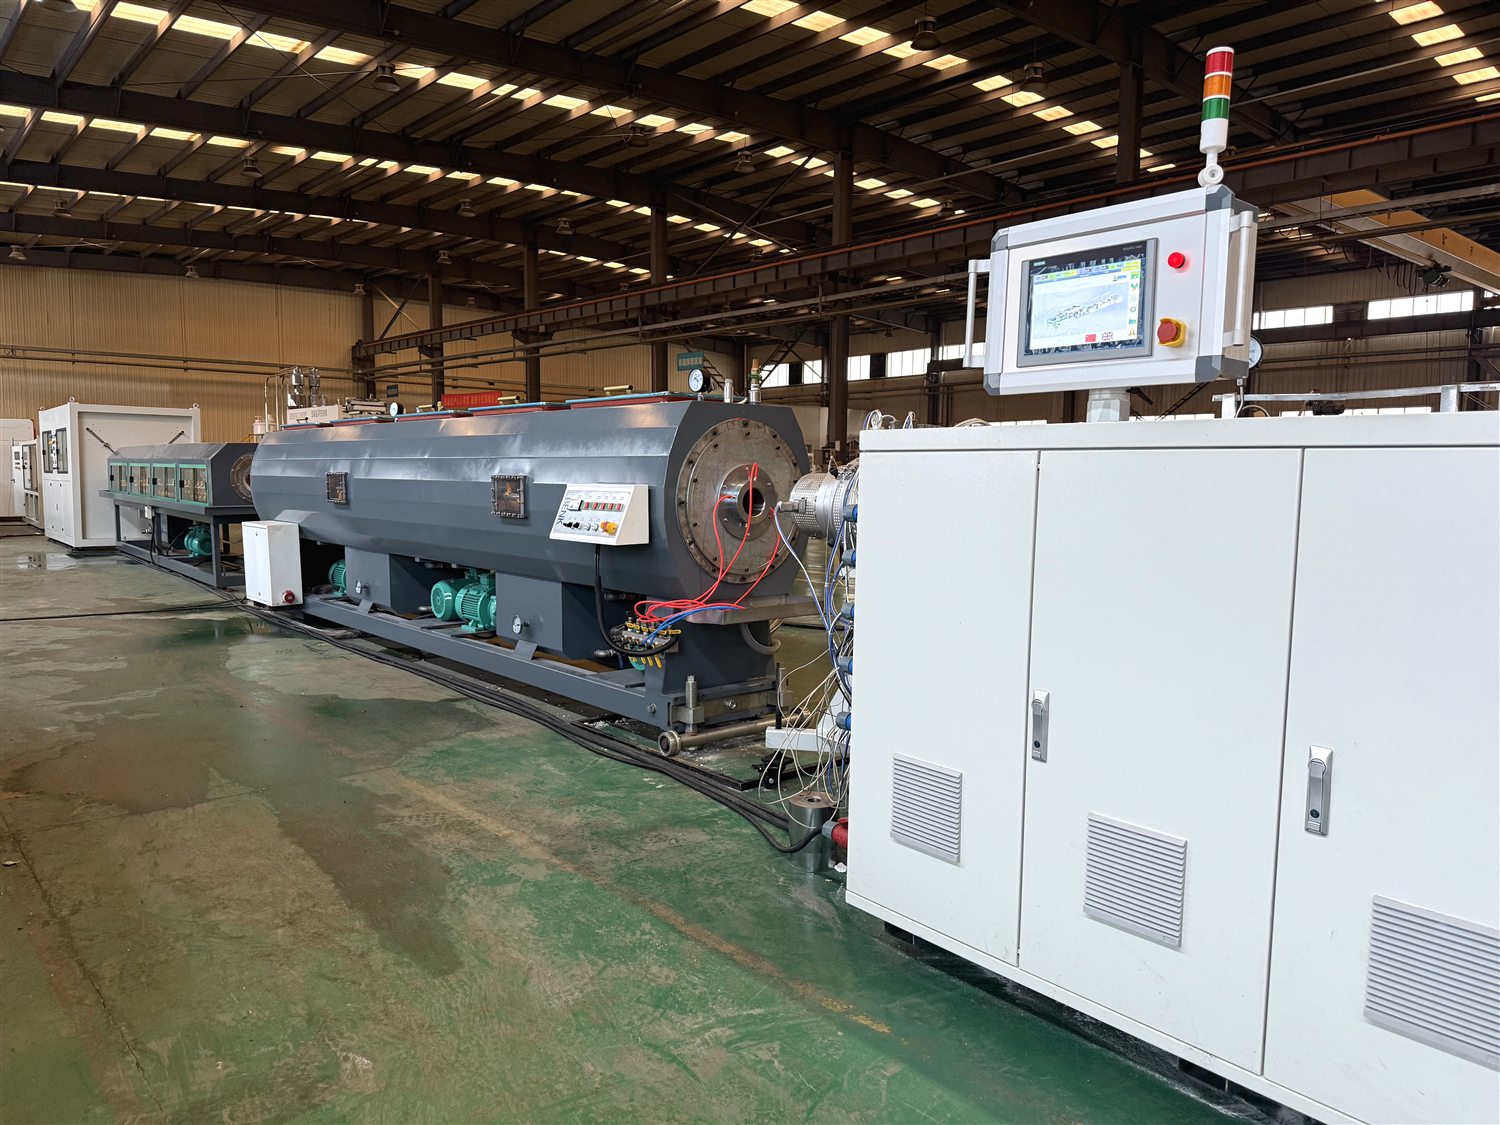
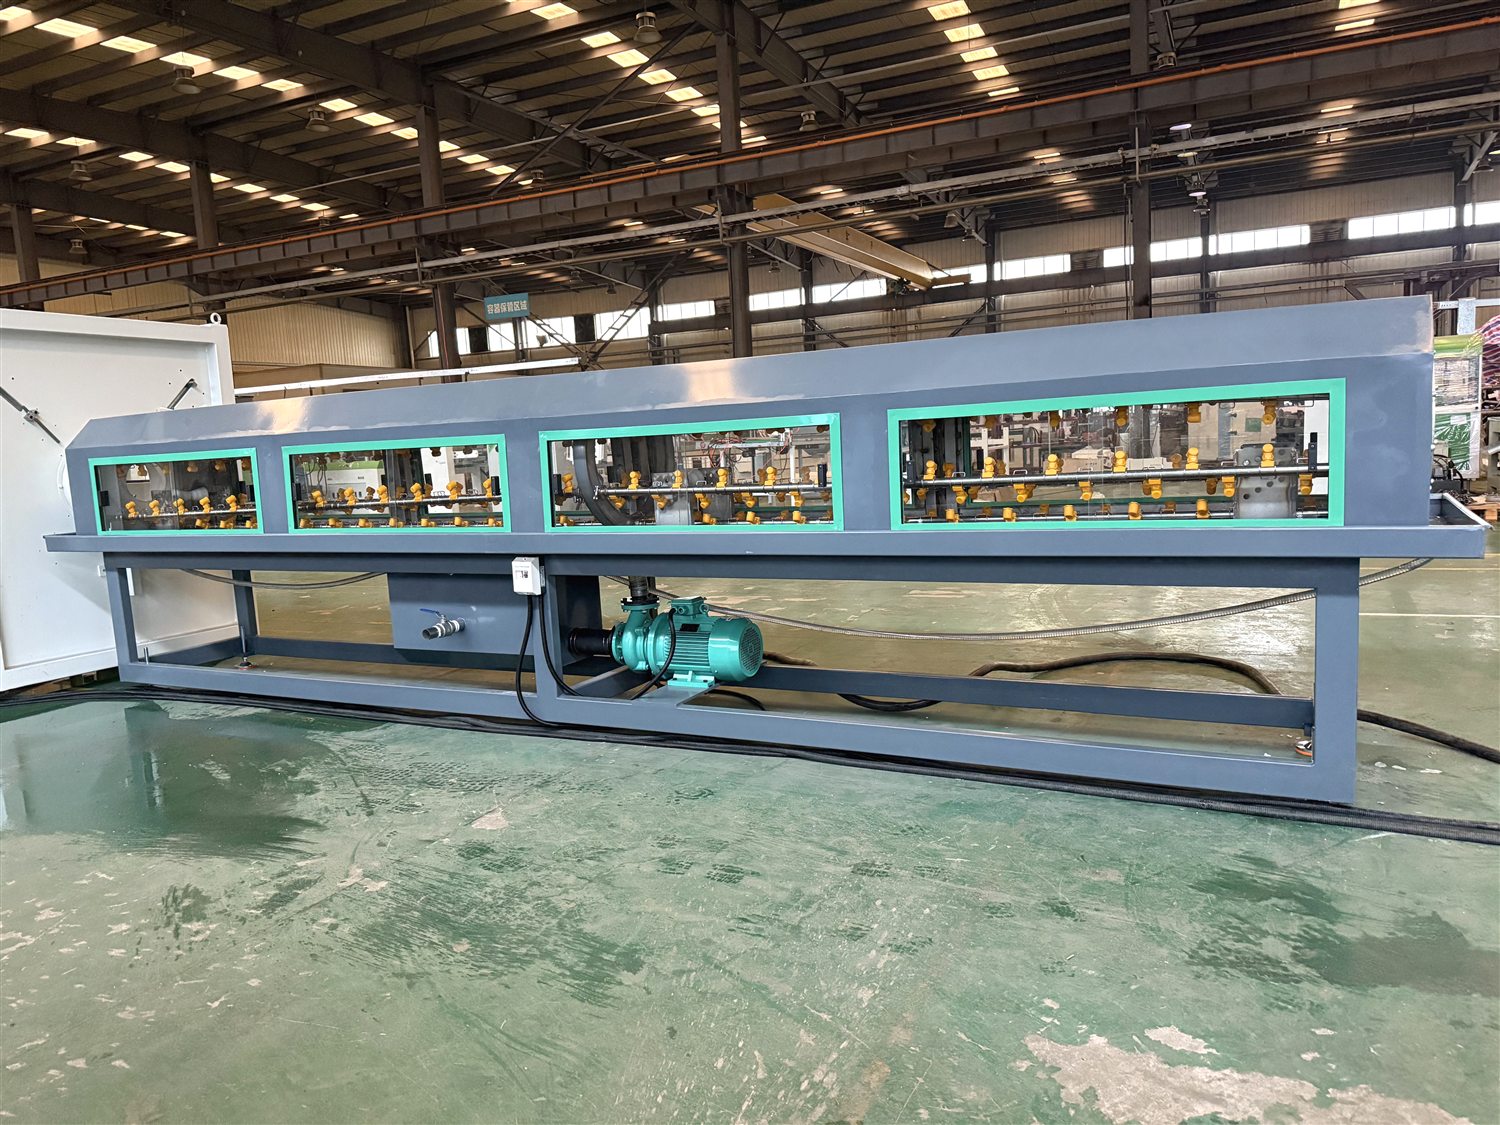
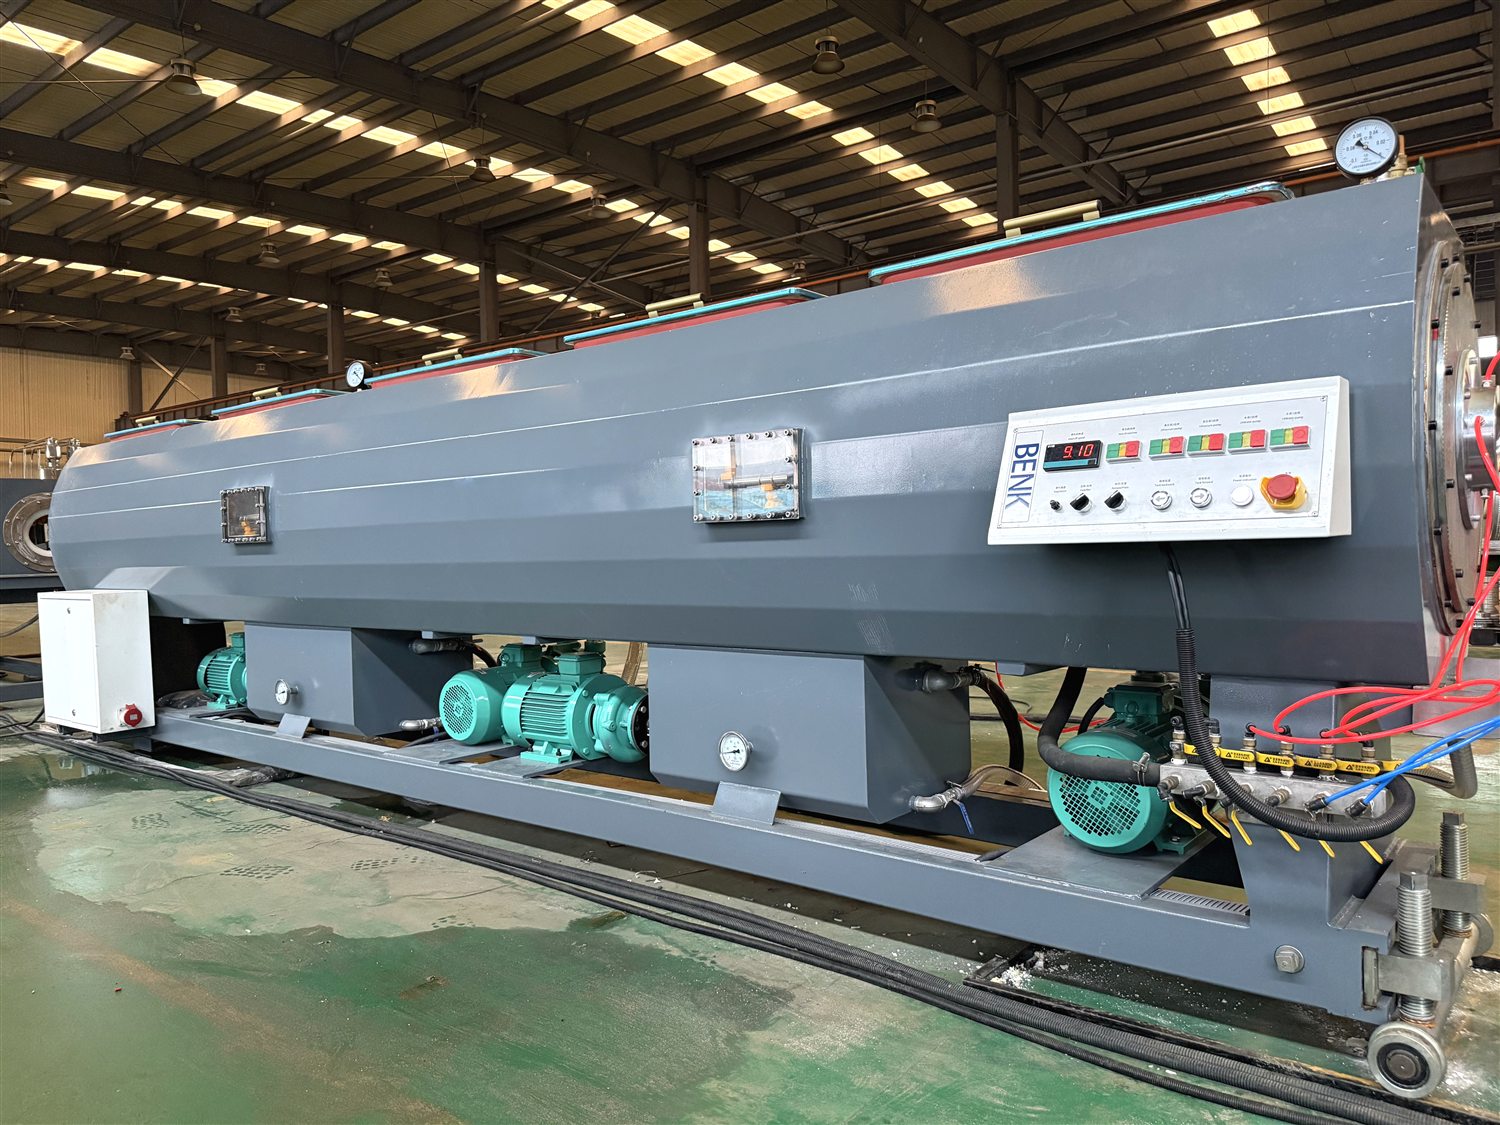
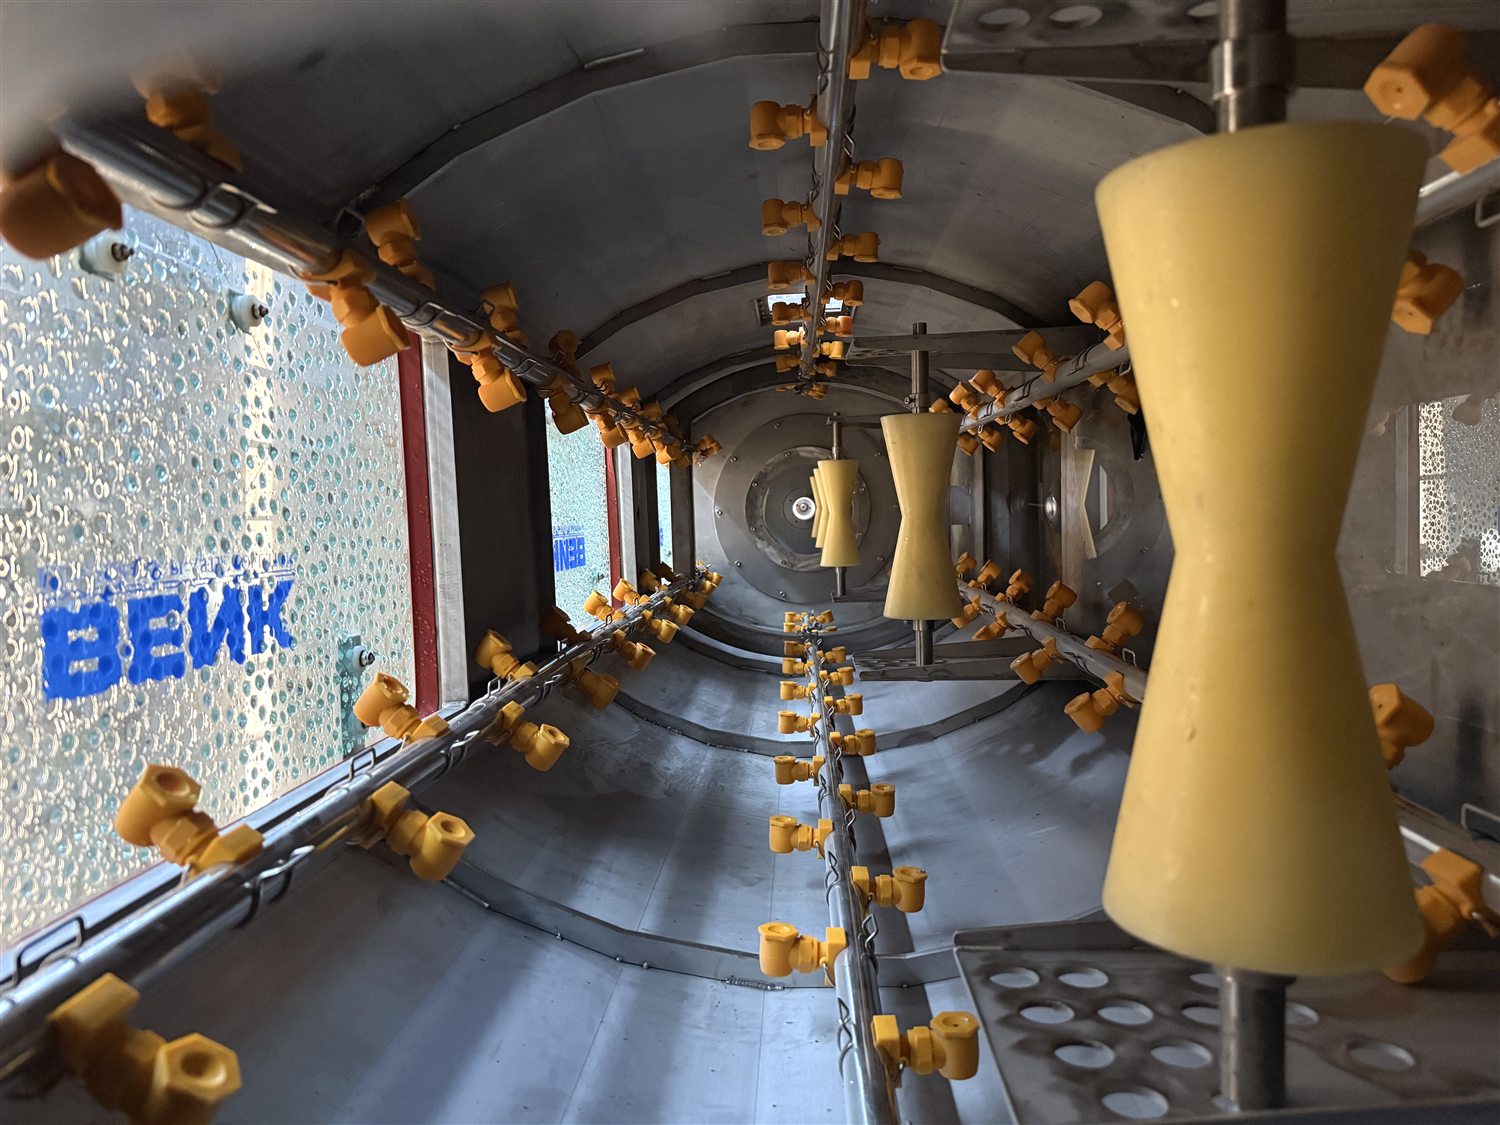
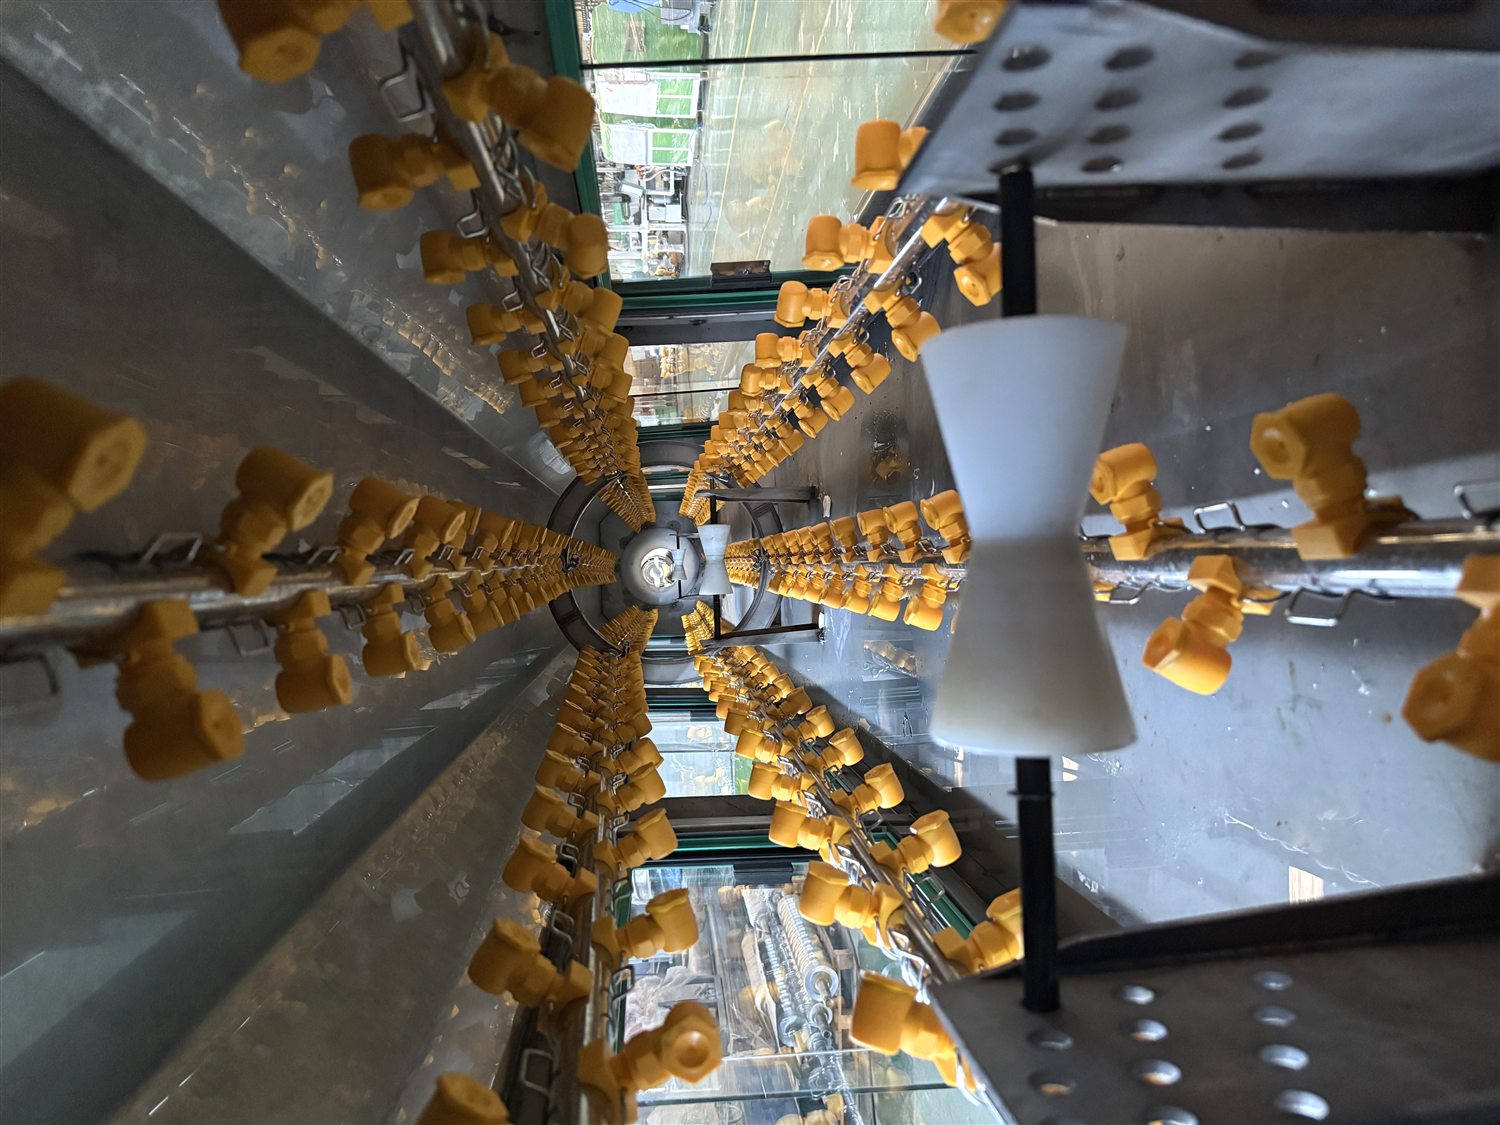
This 160-450 mm PVC pipe production line was built for a Korean subsidiary of the Samsung Group. Large diameter PVC pipe is a cooling problem as much as an extrusion problem: if the pipe leaves the calibration sleeve too warm it ovalises, and if it cools unevenly the wall thickness drifts. The calibration and spray cooling section on this line was therefore sized for the full 450 mm range, with inline support rollers through the tanks.
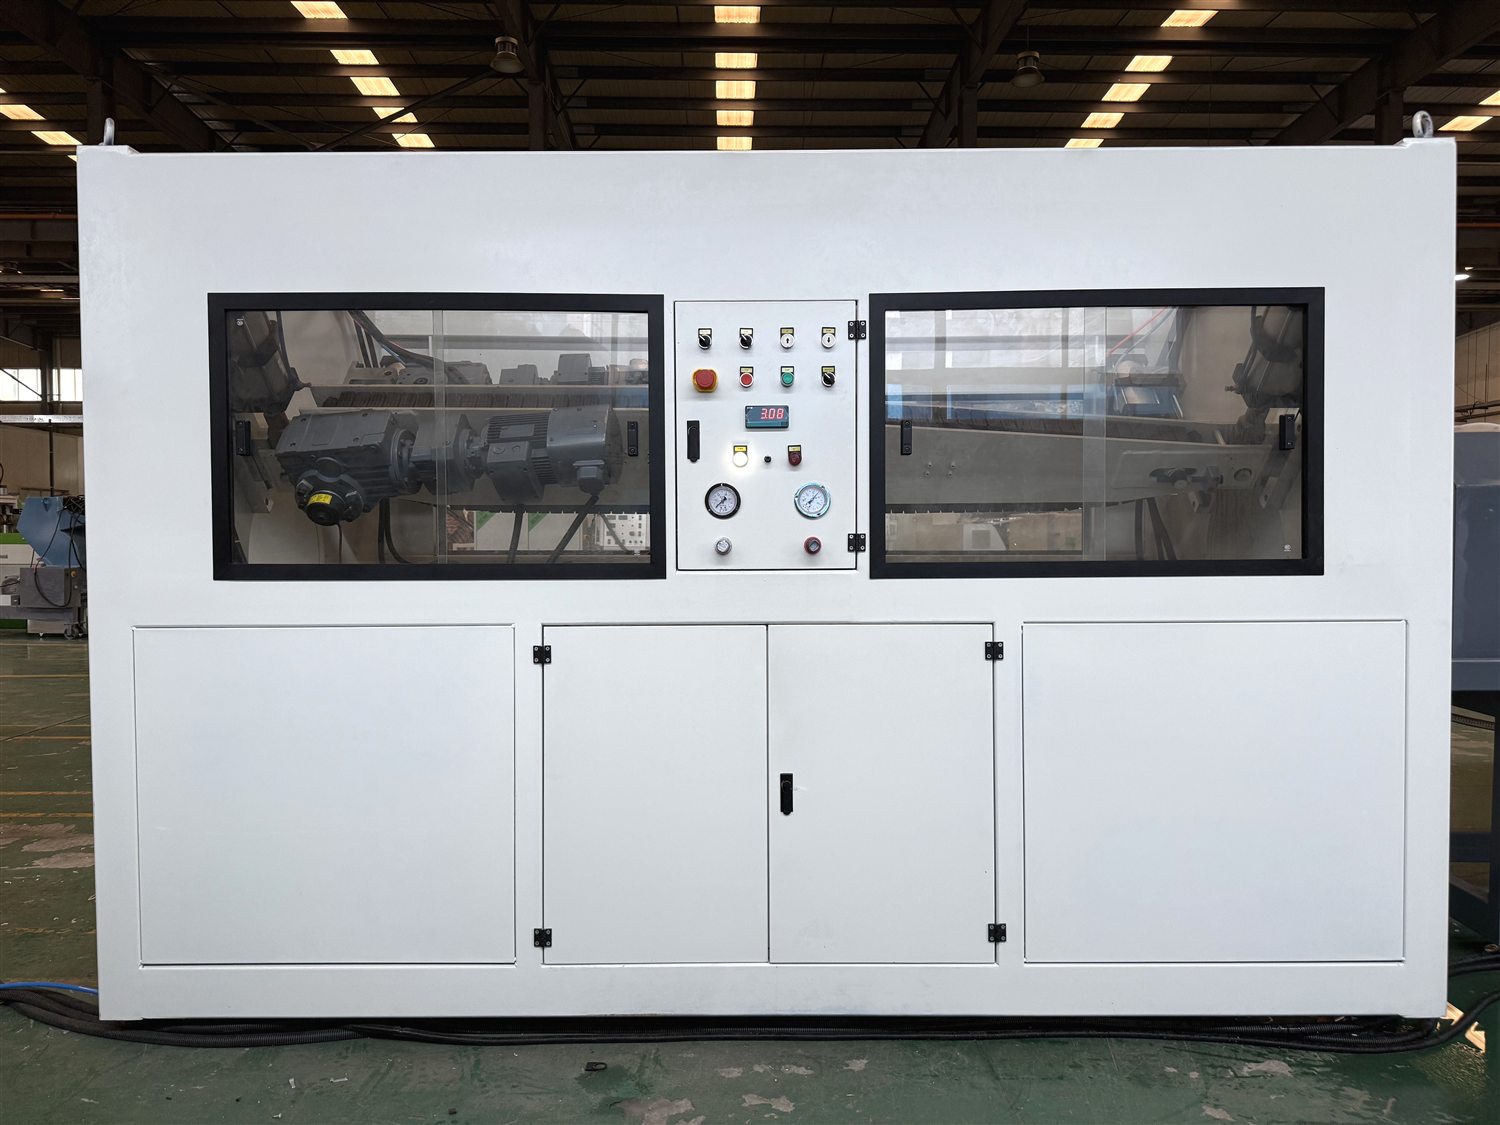
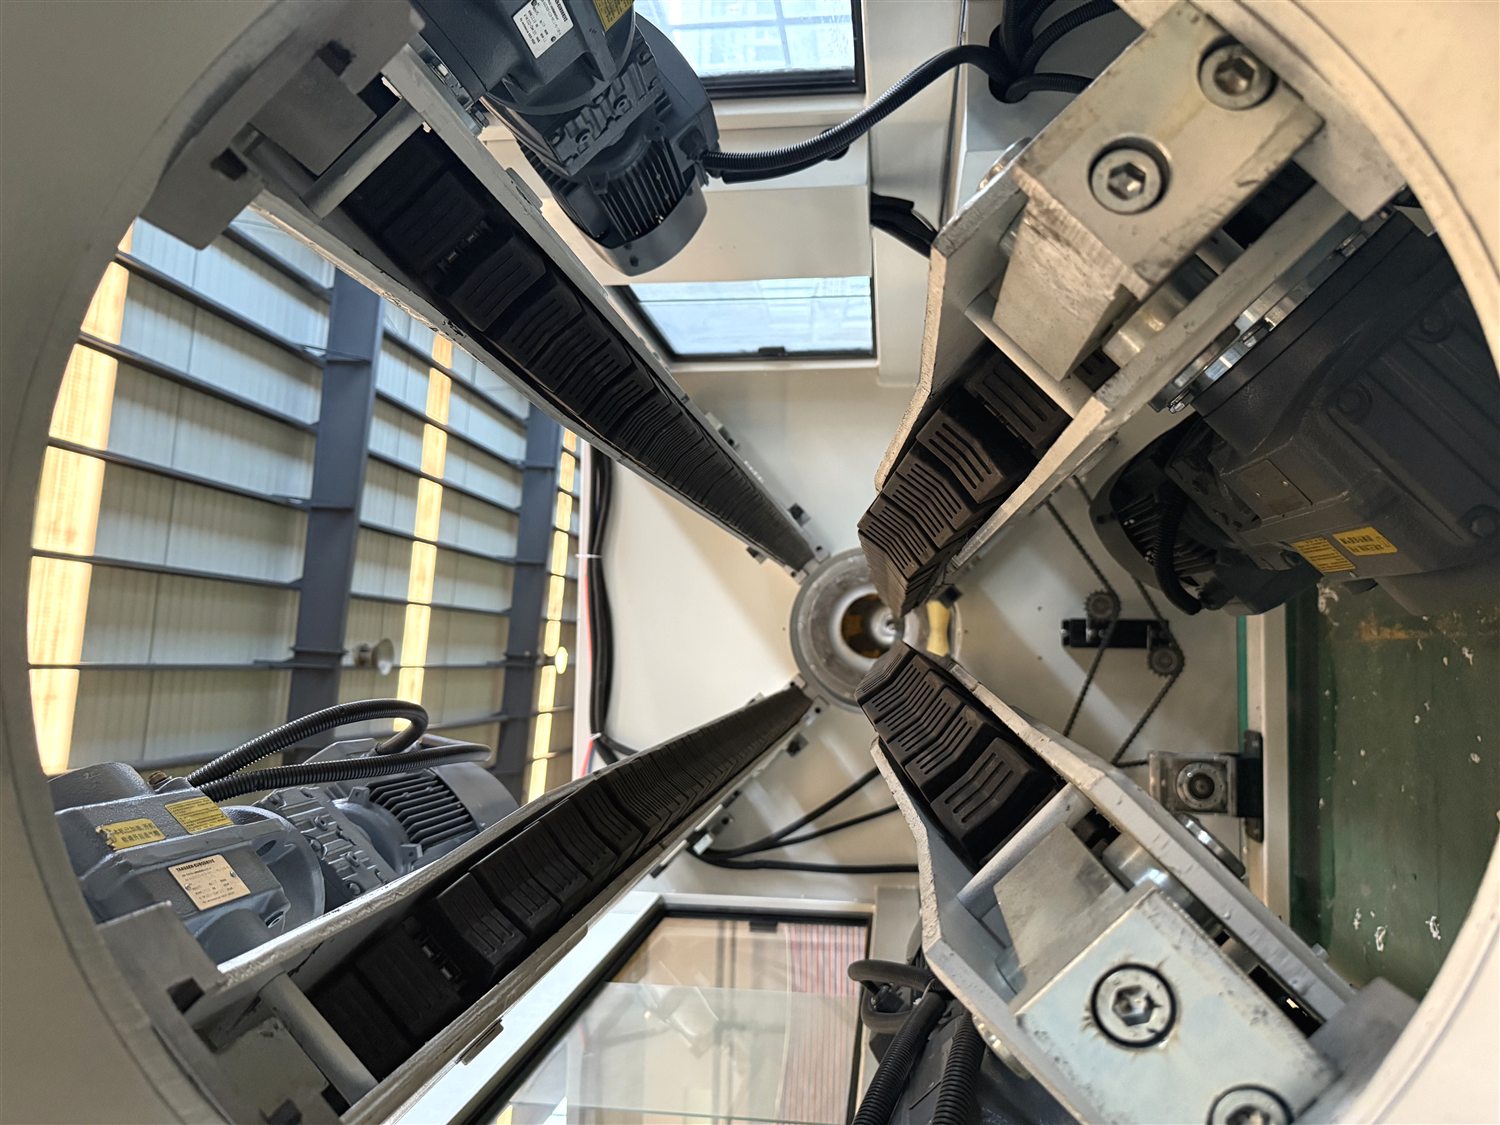
The line is completed by a four-belt haul-off and automatic cutting, so a full 450 mm pipe is pulled without slippage and cut square. Like the rest of our large diameter PVC pipe extrusion lines, it was assembled, wired and run at our workshop in Zhangjiagang before it was packed for Korea.
BENK supplies PVC pipe making machines from 16 mm irrigation pipe through to 630 mm large diameter PVC pipe production lines, including double and four cavity lines for small diameters and single cavity lines with long calibration sections for large diameters. Send us your pipe sizes and target output and we will recommend the extruder and line length that fit.
Send us your material, product size and target capacity -we will come back with a line proposal.