WDP-07 · Texture and wood grain
Embossed WPC Door Panel Production Line: Make the Texture Repeat, Not Just Look Deep
Deep grain can sell the first sample and create a headache in the second container. What matters is whether the pattern has the same depth, gloss and registration on every panel and after the film or coating is added.
Technical review: BENK Machinery · Updated 6 November 2026
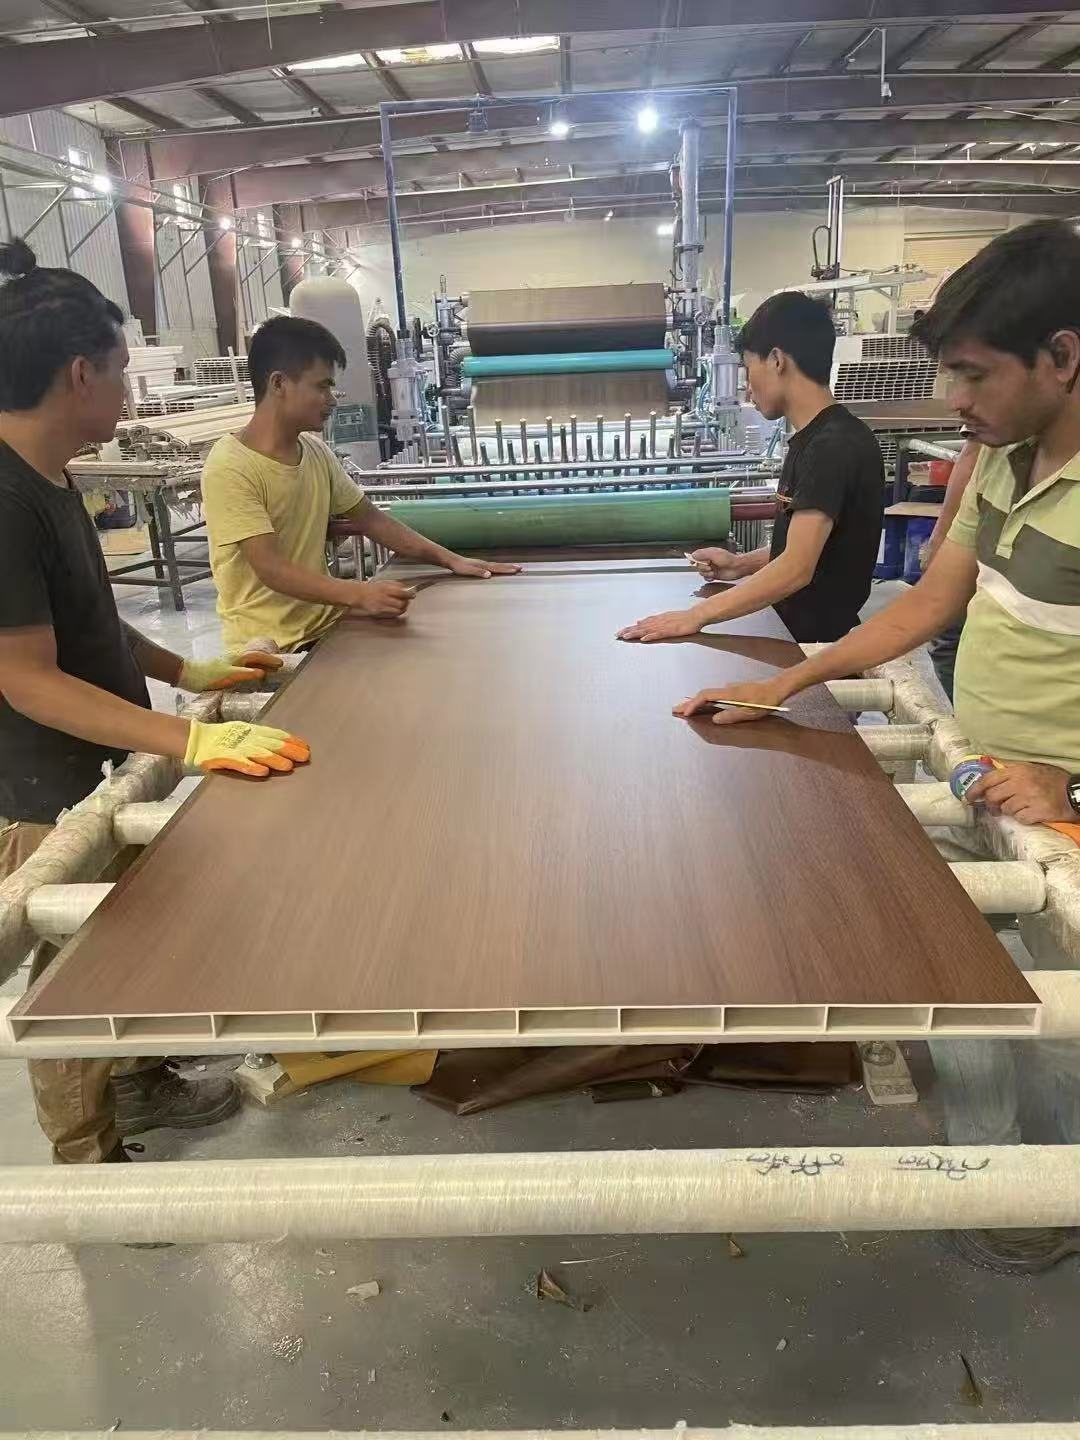
Embossing changes the way a WPC door panel catches light. A shallow pattern can look flat, while a deep pattern can hide small surface waves. The production challenge is to keep the texture consistent as line speed and melt temperature change.
This guide is for buyers who want a textured WPC door board that still looks controlled after cutting, packing and installation. The line, the pattern and the downstream cooling have to be planned together.
What controls texture depth
The panel has to reach the embossing roller at the right temperature and surface hardness. If the face is too hot, the pattern can become glossy or stick. If it is too cool, the roller may only mark the surface without forming a durable texture.
Roller pressure, roller temperature and line speed all affect the result. So does the substrate. A panel with uneven thickness will not sit evenly under the roller, and one edge may show a weaker pattern than the other.
- Pattern depth changing from edge to edge
- Gloss differences across the face
- Roller marks or sticking
- Texture flattening after packing
- Pattern misalignment on long panels
The line conditions behind a repeatable pattern
The die and calibration section must deliver a flat panel with stable thickness before embossing starts. A separate preheat zone can help bring the surface to the right condition without overheating the core. The roller then needs controlled pressure and temperature through the full panel width.
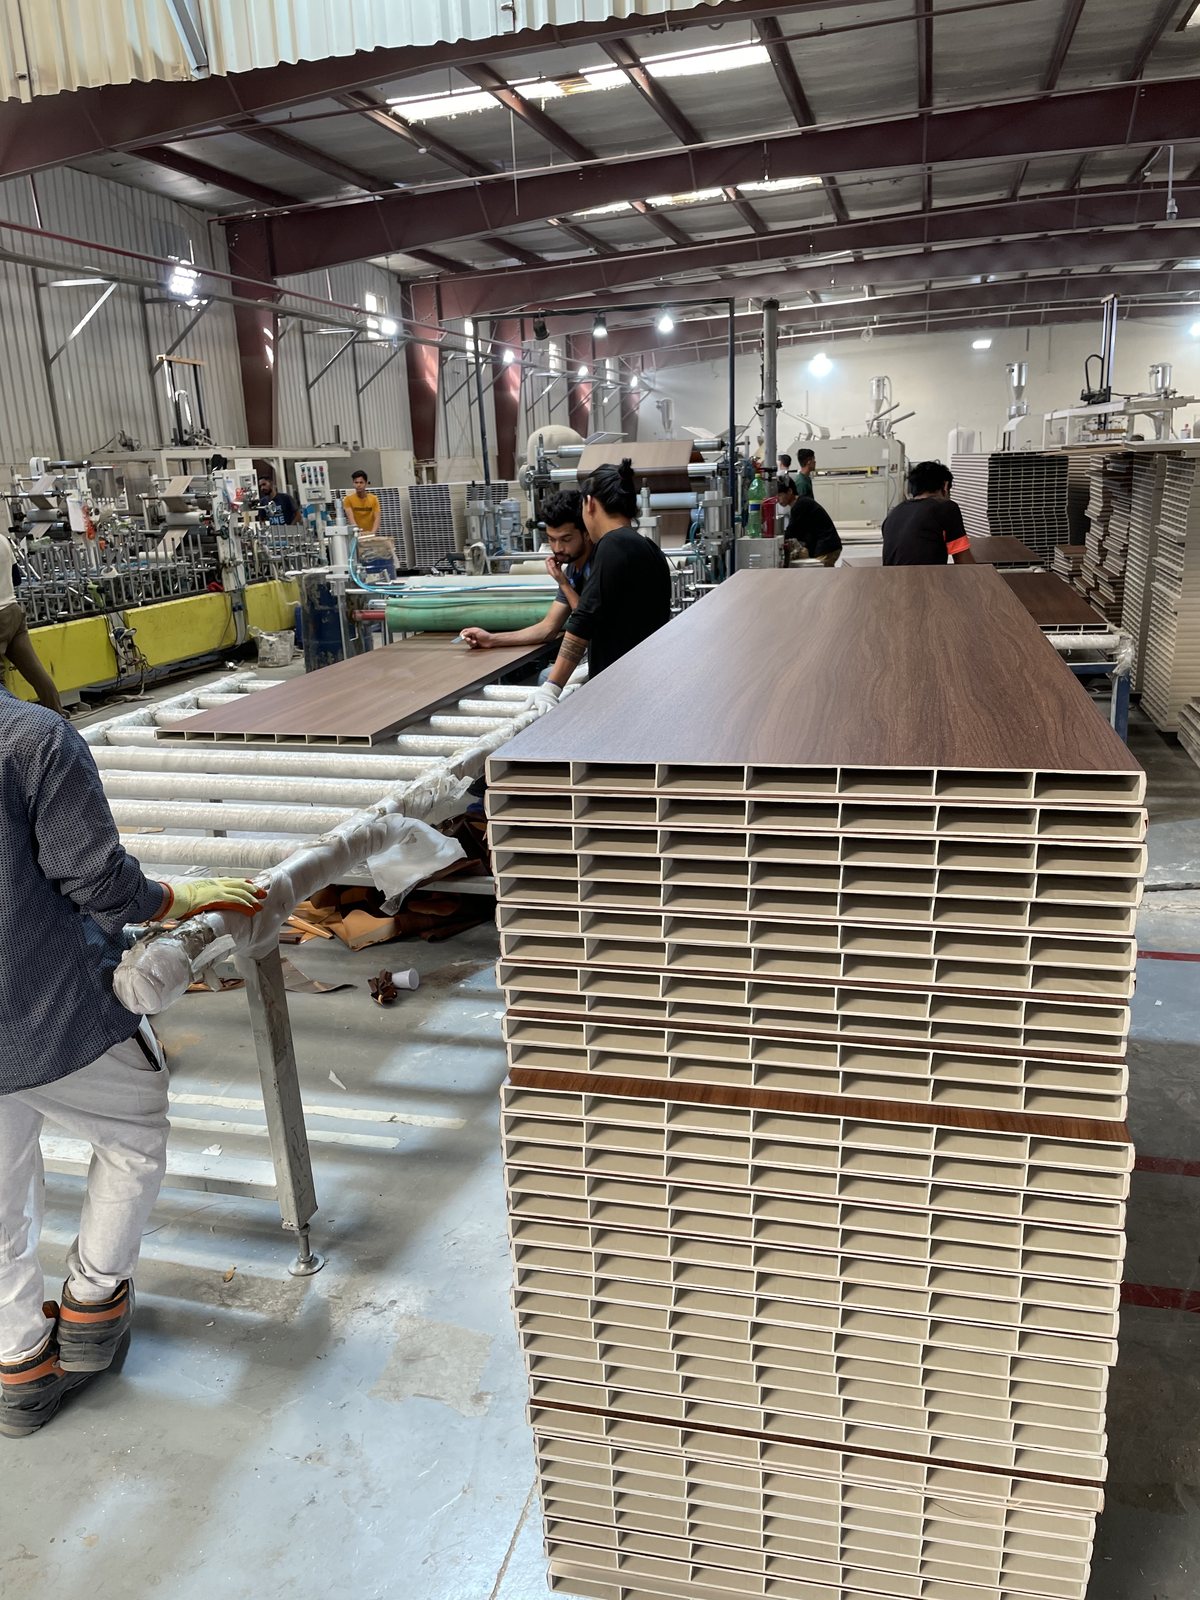
Cooling after embossing is just as important. If the panel is stacked while the surface is still soft, the pattern can change under its own weight. The run-out table and stacking method should protect the new texture.
How BENK approaches a textured panel project
BENK can review the base door-board line with the intended embossing route. The die, calibration table, haul-off and downstream handling are arranged so the panel reaches the texture station in a stable condition. The exact embossing unit depends on the pattern and whether the finish is inline or offline.
Before shipment, a trial should include the actual pattern roller, the production formulation and the intended line speed. The approved sample should be checked under the same lighting conditions used by the final customer.
- Base panel flatness agreed before embossing
- Preheat and roller settings recorded in the trial
- Haul-off speed kept stable through the run
- Cooling and stacking arranged to protect the pattern
- Approved texture sample kept as the production master
Production sequence
From material preparation to finished panel
- 01
Approve the pattern
Select the grain, depth and gloss target from a physical sample.
- 02
Confirm the base panel
Check thickness and flatness before adding texture.
- 03
Set the surface temperature
Bring the face to the embossing window without overheating the core.
- 04
Set roller pressure
Balance pressure across the panel width.
- 05
Emboss at stable speed
Keep line speed steady while the pattern is transferred.
- 06
Cool the surface
Support the panel until the texture is stable.
- 07
Pack without marking
Use a clean interleaf or protective film where needed.
Reference window
Reference specification and planning range
The figures below are a starting point for discussion. The final line specification should follow the approved panel drawing, material formula and trial result.
| Item | Reference / planning note |
|---|---|
| Base panel | WPC door board with stable thickness and flatness |
| Texture options | Wood grain, fine grain, brushed effect or customer-approved pattern |
| Embossing method | Roller-based, inline or offline depending on the project |
| Key controls | Surface temperature, roller temperature, pressure and line speed |
| Cooling | Controlled run-out and stacking after texture transfer |
| Inspection | Pattern depth, gloss, registration, scratches and flattening |
How BENK fits the project
Where the BENK line supports the result
BENK can plan the extrusion and handling section around an embossed WPC door panel route. The texture unit and pattern trial should be confirmed with the actual formulation and panel size before the final scope is agreed.
Buyer checklist
What to settle before you compare quotations
- Ask for a textured sample made on the intended substrate, not a generic plastic sheet.
- Check the pattern at both edges and the centre of the panel.
- Confirm whether the texture will be coated, printed or left exposed.
- Record roller temperature and pressure in the trial report.
- Inspect a panel after 24 hours and after packing to check for flattening.
Questions buyers ask
WPC door panel line FAQ
Can any WPC door panel be embossed?
The substrate needs a suitable surface and stable thickness. Formulations with a very hard or very glossy surface may need a different preheat and roller setup.
Will the texture look the same after film lamination?
No. Film can soften or fill the texture. If the final product is laminated, the texture and film should be tested together.
What causes gloss variation on an embossed panel?
The most common causes are surface temperature changes, roller pressure differences and line-speed variation. A stable trial record helps isolate the cause.
Can BENK supply the embossing unit with the line?
The finishing route can be reviewed with the main line. The exact unit depends on whether the process is inline, offline or carried out by a specialist finishing partner.
Project brief
Tell us the panel, not just the machine.
Send the panel drawing, material formula, target output and factory location. BENK can then review the line configuration against the actual product.