
RTP Line Quality
RTP Quality Control & Traceability
RTP quality depends on stable extrusion, controlled tape tension, repeatable heating, accurate jacket sizing and reliable end-of-line inspection. BENK integrates line control, recipe management, diameter measurement, printing, cutting, coiling and hydrostatic testing equipment into one production flow.
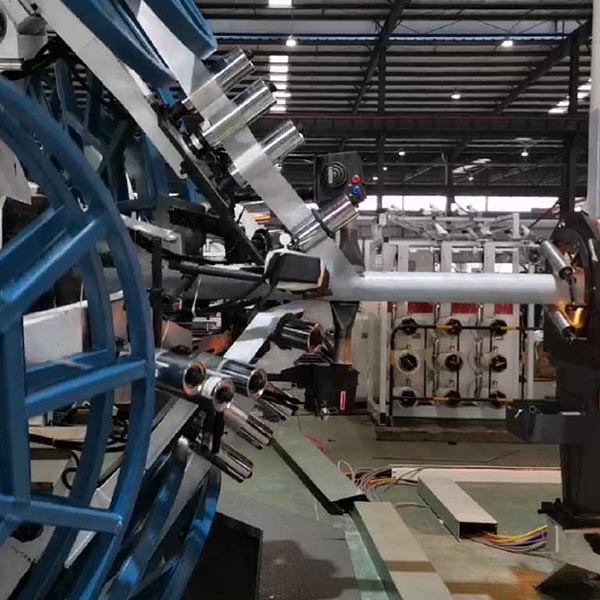
Process controlExtruder speeds, temperatures, line speed and winding recipes are coordinated through the line control system.
Inline measurementDiameter gauge and printer support dimensional control and product marking.
End-of-line testHydrostatic test rig is included in the confirmed line for pressure testing.
TraceabilityRecipe, run data, coil records and test results can be linked to production batches.
What is controlled and recorded
| Parameter | Equipment / function | Recorded value |
|---|---|---|
| Core tube dimensions | SJ65/33 extruder, die, sizing and vacuum cooling | Extruder speed, melt pressure, temperature, line speed |
| Reinforcement schedule | Two winding heads, pay-off and tension control | Tape tension, winding angle, layer count and recipe ID |
| Heating / activation | Preheating oven and adhesive activation oven | Zone temperatures, line speed and alarm status |
| Jacket dimensions | SJ90/30 jacket extruder, cross-head die, vacuum and spray cooling | Extruder speed, temperatures, cooling conditions, diameter |
| Finished pipe size | Diameter gauge and printer | Outside diameter and printed product identification |
| Coil data | Caterpillar haul-off, planetary cutter, double-station coiler | Length, coil number and coil weight where the system supports it |
| Pressure test | Hydrostatic test rig | Test pressure, hold time, result and operator record |
The exact data points and recording depth are agreed with the customer. The line control system supports stable production and traceability, but final pipe qualification and certification remain the pipe manufacturer’s responsibility.
Confirmed line equipment supporting quality
Diameter gauge and printerInline dimensional feedback and product identification.
Hydrostatic test rigPressure-test station included in confirmed line scope.
MCC and control roomMotor control, line power distribution and central control.
Control desk and HMIOperator interface, recipes, alarms and line status.
Planetary cutterControlled cut-to-length before coiling.
Double-station coilerContinuous coiling and coil changeover.
Quality records and operating discipline
Recipe controlValidated recipes reduce operator variation when changing pipe size or reinforcement schedule.
Alarm historyHelp operators identify temperature, tension, drive or safety deviations.
Batch / coil linkageLink production data to coil numbers and test results where the scope includes it.
Maintenance recordsKeep inspection and spare-parts records to protect long-term production stability.
What to include in the quality scope
- Pipe size and wall-thickness tolerances
- Winding angle and layer-count verification
- Tape tension records
- Temperature and line-speed records
- Diameter and ovality limits
- Coil length and weight tolerance
- Hydrostatic test pressure and hold time
- Batch/coil numbering method
- Alarm and maintenance records
- Customer-specific traceability format
Define the quality records before production
Send the pipe specification, test plan and traceability requirements. BENK will confirm the control, measurement and data scope for the line.