RTP Equipment
RTP Heating & Jacket Extrusion
Controlled heating and outer jacket extrusion are critical for bonding the reinforcement package and protecting it in service. BENK configures the heating section, jacket extruder, die, sizing and cooling around the pipe materials and line speed.
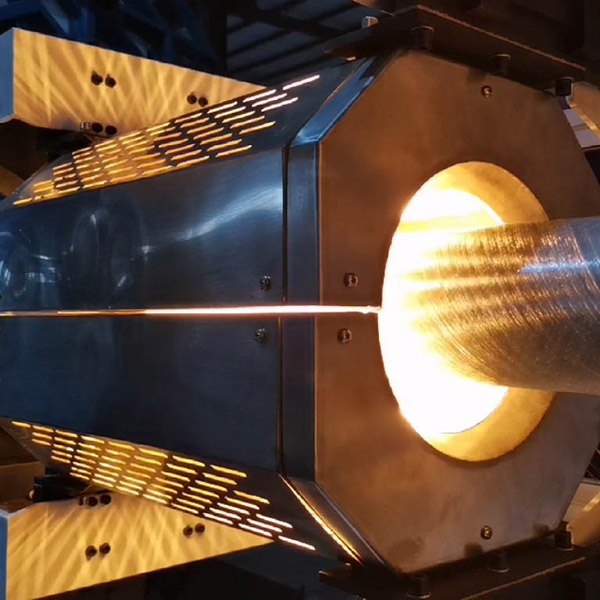
The heating section
The heating section brings the liner and reinforcement to the temperature required for the next process step. Depending on the material system, the line may use hot air, infrared or another qualified heating method. The goal is controlled surface activation and thermal history, not simply the highest possible temperature.
Insulated panels reduce heat loss and help maintain a stable temperature profile.
Air distribution and exhaust are designed to avoid hot spots and uneven heating.
Thermocouples, controllers and optional product temperature measurement support repeatability.
Heating energy is adjusted as the line accelerates or changes product size.
Common error to avoid: an RTP heating oven is not a thermoset curing oven. It must be set for the thermoplastic material system and the required bonding window, not a generic “cure” temperature.
Jacket extrusion and cooling
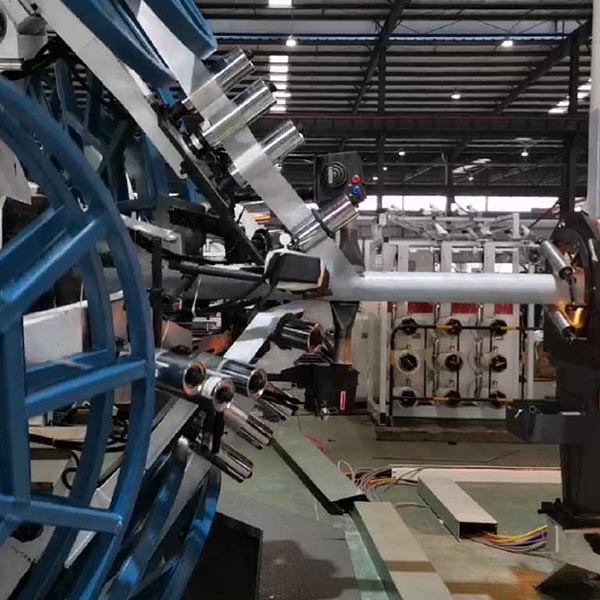
The outer jacket encapsulates the reinforcement and provides mechanical and environmental protection. A dedicated extruder, crosshead/die, vacuum sizing and cooling section are configured for the jacket material and pipe diameter.
- PE, PA or other qualified thermoplastic jacket materials
- Vacuum sizing and multi-stage spray cooling
- Diameter and wall-thickness monitoring options
- Haul-off and tension control matched to the coiler
- Closed-loop line speed and process data logging
Process inputs we need
| Item | Details |
|---|---|
| Pipe construction | Liner material, reinforcement type, tape width, layer count, jacket material |
| Dimensions | Inside diameter, outside diameter, liner wall, jacket wall and tolerance |
| Process window | Target surface temperature, heating method, line speed and cooling requirement |
| Output | Target kg/h or m/min, operating shift pattern and expected product mix |
| Verification | Bond strength, dimensional inspection and production traceability requirements |
Heating and jacket process settings must be qualified for the specific pipe design. BENK confirms the machine scope and control concept in the technical proposal; final product qualification remains with the pipe manufacturer.
Match heating and jacket extrusion to the pipe design
Send the liner, tape and jacket materials, pipe dimensions and target line speed. We will define the heating zones, extruder, die and cooling section.