
RTP Line Service
RTP Line Commissioning & Training
A complete RTP line is a coordinated process, not a group of independent machines. BENK supports the transition from factory acceptance and installation through dry running, material trials, process optimization, operator training and production handover.
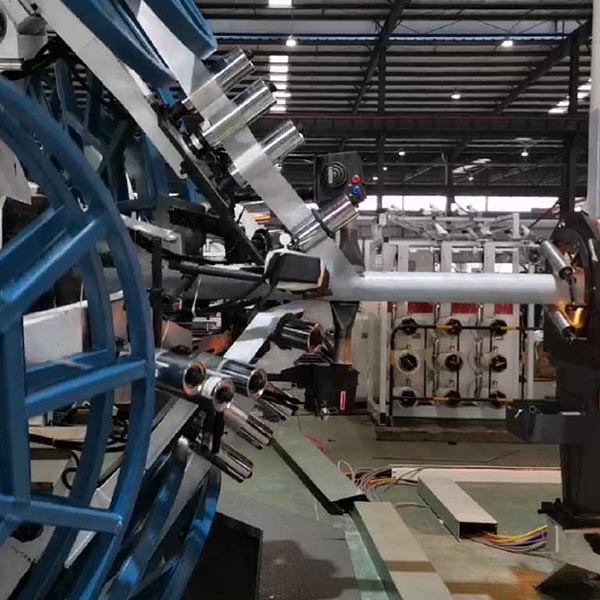
Commissioning sequence
Confirm machine build, rotation, sensors, safety interlocks, control logic and agreed test points before shipment.
Verify foundation, alignment, utilities, power, compressed air, water, drainage and material handling.
Run drives, heaters, winding axes, haul-off, cutter and coiler without material; confirm interlocks and emergency stops.
Establish core tube dimensions, preheat/activation settings, tape tension, jacket thickness and cooling conditions.
Tune line speed, winding angle, layer sequence, temperatures and coiler tension to the agreed product.
Confirm operating recipes, quality records, maintenance routines and spare-parts recommendations.
Training modules
| Module | Content | Who should attend |
|---|---|---|
| Line operation | Start-up, shutdown, recipe selection, alarms, normal running and emergency procedures | Line operators and shift leaders |
| Core tube extrusion | SJ65/33 extruder, die and sizing, vacuum cooling and first haul-off | Extrusion operators |
| Reinforcement winding | Tape loading, ±54.7° balanced winding, tension control, layer recipes and defect checks | Winding operators and process engineers |
| Heating and jacket | Preheat, adhesive activation, SJ90/30 jacket extruder, die, cooling and diameter control | Extrusion and process teams |
| Cutting and coiling | Haul-off, cutter, double-station coiler, coil geometry and handling | Downstream operators |
| Maintenance and safety | Routine inspection, lubrication, guards, interlocks, lockout procedures and spare parts | Maintenance and safety staff |
What is confirmed before commissioning
- Pipe size matrix and pressure class
- Liner, reinforcement and jacket materials
- Line layout and utility requirements
- Installed power: 401.5 kW
- 33 equipment items / 34 machines
- Target output: 120–350 kg/h
- Line speed: 0.5–8 m/min
- Coil size and handling method
- Quality records and acceptance criteria
- Operator staffing plan: 2–3 people per shift
Commissioning duration and the exact acceptance tests depend on the scope, site readiness and product trial plan. The schedule is agreed in the project execution plan before shipment.
Plan training before the line arrives
Share the pipe product plan, shift structure and site utilities. BENK will align the commissioning sequence and training modules with the line configuration.